|


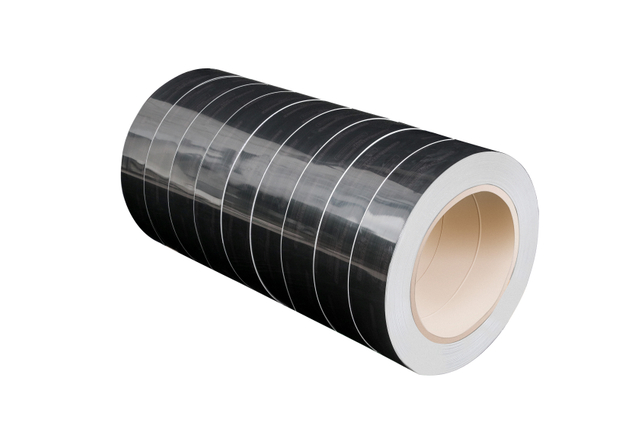
High Glossy Aluminum Coil
Dingang
7606125000
| Quantity: | |
|---|---|
3003 0.3mm PE-coated aluminum sheet is a thin-gauge aluminum packaging material for semi-rigid food containers, trays, lids, container components and compatible laminated packaging structures that require good formability, corrosion resistance and a controlled coated surface.
The primary product specification is AA3003 aluminum with a nominal thickness of 0.30 mm and width of 1300 mm. The broader listed production range covers 0.10–2.00 mm thickness and 800–2200 mm width, subject to alloy, temper, coating, application and production confirmation.
At 0.30 mm thickness, this material is more accurately described as thin-gauge aluminum sheet or strip rather than conventional aluminum foil. It provides greater rigidity than typical thin container foil and is therefore better suited to semi-rigid packaging components where additional shape retention is required.
For any application involving direct food contact, the exact coating chemistry, coating side, coating weight or film thickness, food type, contact temperature and contact duration must be confirmed before production. Food-contact suitability applies to the complete aluminum-and-coating system rather than the aluminum alloy alone.
Request 3003 Food Packaging Aluminum Price
| Product | 3003 coated aluminum sheet / strip for food packaging applications |
| Primary Alloy | AA3003 |
| Primary Thickness | 0.30 mm |
| Primary Width | 1300 mm |
| Listed Thickness Range | 0.10–2.00 mm; final availability depends on application, alloy, temper and coating |
| Listed Width Range | 800–2200 mm; final maximum width should be confirmed with thickness, coating and supply form |
| Temper Options | O, H12, H14, H16, H18, H24, H26, H32, H34 and application-specific conditions subject to confirmation |
| Surface Finishing | Coated surface; exact coating system must be specified according to packaging use |
| T-Bend Reference | No more than 2T according to the existing coated-aluminum product data; applicability should be confirmed for the selected coating system |
| Existing PVDF Coating Reference | Not less than 25 µm according to the broader coated-aluminum supply data; this value does not by itself establish food-contact suitability |
| Existing PE Coating Reference | Not less than 18 µm according to the existing product data; exact PE chemistry and food-contact suitability must be confirmed for the intended package |
| Packing | Export-standard wooden pallets; eye-to-wall or eye-to-sky configuration for applicable coil shipments |
| Payment Terms | L/C at sight or 30% T/T deposit with 70% balance against the B/L copy according to the listed commercial terms |
| MOQ | 2 metric tons per specification |
| Delivery Reference | Approximately 30–45 days subject to final specification, coating, quantity and production schedule |
| Loading Ports | Shanghai, Ningbo, Qingdao, Tianjin and other agreed ports |
| Existing Application Reference | Semi-rigid food packaging, container components, trays, lids and compatible laminated packaging; suitability must be matched to thickness and coating system |
AA3003 is an aluminum-manganese alloy commonly selected where formed packaging components require a practical balance of strength and formability. The appropriate temper depends on forming depth, rim geometry, wall shape and the stiffness required after forming.
At 0.30 mm nominal thickness, the material has substantially greater rigidity than conventional thin food-container foil. This makes it suitable for packaging parts where additional shape retention, handling strength or resistance to local deformation is required.
3003 aluminum provides practical corrosion resistance for many packaging applications. Where food, salt, acids, fats or other ingredients may contact the package, the correct food-contact coating or lacquer should be selected for the specific product and process.
Depending on temper and tooling, the material can be evaluated for stamping, shallow drawing, bending, lid forming and other compatible converting processes used to manufacture semi-rigid packaging components.
Discuss Your Food Container Design
Conventional aluminum foil for disposable food containers is generally much thinner than 0.30 mm. The 0.30 mm specification should therefore be selected when the package requires greater stiffness or when the material forms part of a more rigid packaging component.
| Selection Factor | 0.30 mm 3003 Sheet / Strip | Conventional Thin Container Foil |
| Material Character | Thin-gauge semi-rigid sheet or strip | Flexible to semi-rigid foil |
| Rigidity | Higher | Lower |
| Typical Conversion | Stamping, shallow drawing, lid or container-component forming | High-speed foil-container forming, flexible or lightweight semi-rigid packaging |
| Selection Priority | Shape retention, stiffness, formed-part durability | Low material weight, flexibility and high-speed converting |
When the aluminum layer is continuous and undamaged, aluminum provides an effective barrier to light and gases. The coating should therefore not be described as the only source of oxygen or light barrier performance.
The coating or polymer layer can add functions such as heat sealing, protection against specific food ingredients, adhesion to other layers, decoration, printability or improved resistance to moisture and handling, depending on its exact chemistry.
Barrier performance of the finished package also depends on formed corners, seams, seals, pinholes, laminate construction and closure design. Shelf-life claims should therefore be validated on the complete package with the intended food product.
The abbreviation PE can have different meanings in different aluminum markets. In food packaging it may describe a polyethylene layer or related sealing structure, while in general prepainted aluminum supply it may be used for polyester paint. These systems are not interchangeable.
For packaging orders, specify the exact coating chemistry, manufacturer or formulation reference where applicable, coating side, film thickness or coating weight, curing condition and whether the coated face will directly contact food.
| Coating Requirement | Information to Confirm |
| Coating Chemistry | Polyethylene layer, polyester coating, food-contact lacquer, heat-seal lacquer or another approved system |
| Coated Side | Single side or double side and identification of the food-contact face |
| Coating Amount | Dry-film thickness, coating weight or laminate thickness according to the coating system |
| Heat-Seal Requirement | Seal temperature, dwell time, pressure and target seal strength where heat sealing is required |
| Food Type | Dry, aqueous, acidic, fatty, salty or other intended food categories |
| Contact Conditions | Filling temperature, retort or oven exposure if any, storage temperature and expected contact duration |
| Documentation | Declaration, migration data or other compliance documentation appropriate to the destination market and intended use |
A 3003 aluminum substrate does not automatically make the finished coated sheet suitable for every food-contact application. Compliance depends on the complete surface system and the intended conditions of use.
For the United States, the applicable food-contact requirements should be confirmed for the specific resinous or polymeric coating, formulation and intended food-contact conditions. Where a coating is evaluated under applicable food-contact provisions, the exact approved formulation and conditions of use must be followed.
For European-market packaging, the finished material should satisfy the applicable general food-contact requirements and any additional requirements that apply to the specific coating, plastic layer or packaging construction.
Buyers should therefore request documentation for the exact production coating rather than relying on a generic statement such as “food grade,” “FDA” or “EU compliant.”
Discuss Food-Contact Coating Requirements
Temper directly affects forming depth, springback, rigidity and the ability of a finished container or lid to retain its shape. The broad supply list includes O through several H tempers, but they should not be treated as interchangeable.
| Temper Direction | Typical Selection Consideration |
| O Temper | Higher ductility where deeper forming is required and final rigidity requirements are lower |
| H14 / H16 | Intermediate work-hardened conditions that can be evaluated where additional stiffness is required |
| H22 / H24 | Common starting points for semi-rigid formed aluminum packaging requiring a balance of formability and shape retention |
| H26 / H18 | Higher-strength conditions for shallower forming or components requiring more rigidity; forming limits should be validated |
The 0.30 mm gauge can be evaluated for relatively rigid trays or container components where greater wall stiffness is required than with conventional thin disposable container foil.
Coated 3003 stock can be evaluated for compatible stamped or formed lids where alloy temper, coating flexibility, closure geometry and sealing system have been validated together.
Semi-rigid aluminum components can be used in suitable takeaway, catering and prepared-food packaging where the finished structure requires additional stiffness and a coated surface.
The aluminum can form part of a laminated or composite structure where the selected coating or adhesive system is compatible with the adjacent polymer, paper or other packaging layer.
For chocolate, candy and chewing-gum packaging, a 0.30 mm sheet is more appropriate for rigid or semi-rigid components than for conventional flexible wrappers. The final package construction should determine whether this gauge is suitable.
Stamping performance depends on temper, material thickness, blank geometry, draw depth, tooling radius, lubrication and coating flexibility. A representative forming trial should be completed for a new package design.
Rolled, curled or folded rims can place significant local strain on both the aluminum and coating. The finished rim geometry should be checked for cracking, coating damage and dimensional consistency.
If the package requires heat sealing, the sealing function must come from a compatible heat-seal layer, lacquer, adhesive or polymer structure. Seal performance should be validated using the intended lid, flange, sealing temperature, pressure and dwell time.
Stable width and controlled burr are important for automatic feeding, blanking and high-volume forming. Buyers should provide the required usable width and edge tolerance for the converting line.
Confirm AA3003 and the approved temper before production because forming performance and finished rigidity vary significantly with material condition.
For the primary SKU, confirm 0.30 mm thickness and 1300 mm width together with the required dimensional tolerances.
Flatness and coil shape affect feeding and blanking. Edge wave, center buckle or unstable winding can reduce productivity on automated converting equipment.
The material should be free from contamination that could interfere with coating performance, sealing, forming or the intended food-contact surface.
The coating should remain intact through the intended forming operation. Test methods and acceptance limits should be agreed for the actual coating system.
Where the coated face contacts food, verify that the documentation corresponds to the exact production coating, food category and conditions of use rather than to a generic coating family.
For a new container or lid, run the material on the intended tooling and check forming, coating condition, dimensions, sealing and finished-package performance before bulk approval.
Request Material for a Packaging Trial
State whether the material is for a tray, container, lid, cover, rigid insert or laminated packaging component.
The primary product is 0.30 mm thick. If another thickness within the broader listed range is required, provide the forming and rigidity requirements for confirmation.
The primary width is 1300 mm. Provide the converting-line feed width, trimming allowance and tolerance if the finished process requires another dimension.
Choose the temper according to forming depth, finished rigidity and springback. H22 or H24 can be evaluated for many semi-rigid components, while other tempers may be required for different forming conditions.
Do not specify only “PE.” State the exact required coating or laminate type, coated side, coating thickness or weight, color if applicable and functional requirement such as sealing, food protection or bonding.
Provide the food category, filling temperature, storage temperature, contact time, heating or retort conditions and whether the coated surface directly contacts food.
Provide drawing depth, rim design, forming speed and any heat-seal requirements so substrate temper and coating flexibility can be evaluated together.
State the destination market and required food-contact documentation before ordering so the applicable coating and testing requirements can be confirmed.
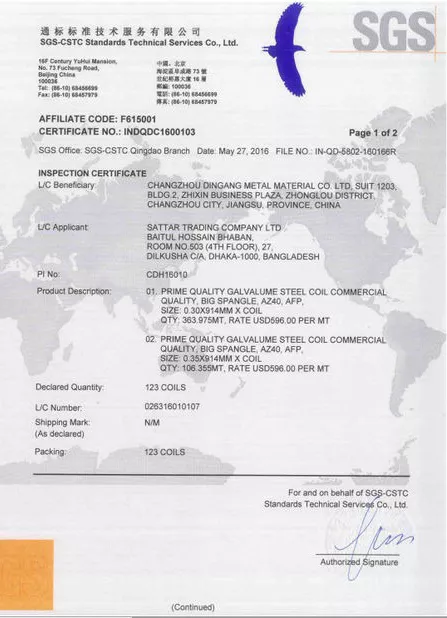
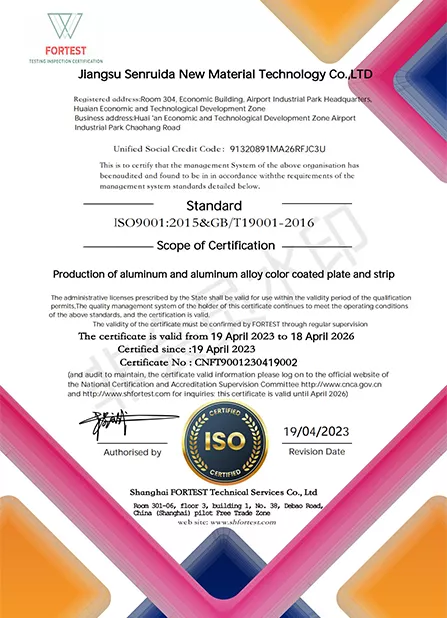
The documents below are the certificate images currently associated with this product. For food-contact procurement, confirm the issuing body, scope, validity and whether each document covers the exact AA3003 substrate, coating formulation and intended food-contact application.
| MOQ | 2 metric tons per specification according to the existing product information |
| Sample | Sample availability can be discussed; the existing product information states that shipping costs are borne by the buyer |
| Payment | L/C at sight or 30% T/T deposit with 70% balance against the B/L copy according to agreed commercial terms |
| Delivery Reference | Approximately 30–45 days subject to final specification, coating and quantity |
| Loading Ports | Shanghai, Ningbo, Qingdao, Tianjin or another agreed port |
| Small Orders | Availability depends on current inventory, coating, thickness and width |
Coated aluminum for packaging should be protected from moisture, surface contamination, edge damage and movement during transportation. Standard export packing uses moisture-resistant wrapping and seaworthy wooden protection according to the shipment format.
Customized packing can be discussed according to coil dimensions, unloading equipment, shipment route and customer handling requirements.
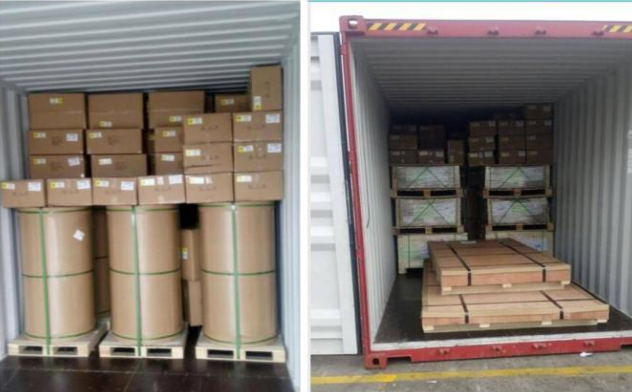
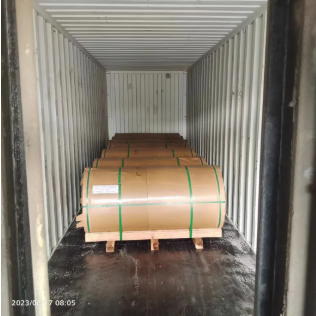
For an accurate quotation, please provide the finished packaging application, alloy and temper, thickness, width, required coating or laminate chemistry, coated side, coating weight or thickness, food type, contact conditions, forming process, heat-seal requirements if applicable, quantity, packing requirement and destination.
For a new food container or lid, providing the finished component drawing and forming parameters can help confirm whether 0.30 mm material is appropriate before sample or bulk production.
Send Your Food Packaging Specification
At 0.30 mm, the product is more accurately described as thin-gauge aluminum sheet or strip rather than conventional aluminum foil. This greater thickness also provides more rigidity for semi-rigid packaging components.
The primary specification is AA3003 aluminum, 0.30 mm nominal thickness and 1300 mm width with a coated surface selected according to the packaging application.
The existing supply data list 0.10–2.00 mm thickness and 800–2200 mm width. Final availability depends on alloy, temper, coating and production requirements.
PE must be defined in the purchase specification. Depending on the product system, it may refer to a polyethylene-based layer or to terminology used for a polyester coating. For food packaging these should never be assumed to be interchangeable.
No. Suitability depends on the exact coating formulation, food type, contact time, temperature and destination-market requirements. Documentation should correspond to the exact coating supplied.
A continuous aluminum layer provides an effective barrier to light and gases. The coating adds application-specific functions such as sealing, chemical protection, printability or bonding depending on its formulation.
Yes, 3003 can be evaluated for food trays and container components. At 0.30 mm, the material is considerably thicker than conventional disposable container foil and is better suited where additional rigidity is required.
Temper depends on forming depth and required finished stiffness. O temper provides greater ductility, while H22 or H24 can be evaluated where a balance of formability and shape retention is required.
Heat sealing requires a compatible heat-seal lacquer, adhesive or polymer layer. The aluminum substrate alone does not create a heat seal. Seal temperature, pressure, dwell time and mating surface should be tested together.
It may be possible with an appropriate food-contact coating, but suitability must be verified for the actual food chemistry, contact duration and temperature. The 3003 substrate alone should not be used to make a universal compatibility claim.
Only when the complete aluminum, coating, seal and package structure is qualified for the required process temperature, pressure, time and food product. A generic PE-coated specification should not automatically be assumed suitable for retort processing.
The existing supply table includes a PVDF coating reference as part of the broader coated-aluminum range. For direct food contact, use only a coating system specifically documented and approved for the intended food-contact conditions.
Required documentation should be discussed before production because it must correspond to the exact coating formulation, intended food type, conditions of use and destination market.
The existing product information lists an MOQ of 2 metric tons per specification.
The existing product information lists approximately 30–45 days. Actual lead time depends on alloy condition, coating, dimensions, quantity and production schedule.
Sample availability can be discussed. For a new package, a production-representative forming and sealing trial is recommended before approving bulk material.
Please provide packaging application, alloy and temper, thickness, width, coating chemistry, coated side, food category, contact temperature and time, forming process, heat-seal requirements, quantity, required documentation, packing requirements and destination.