
 |


8011 H18
DINGANG
7607110000
| Quantity: | |
|---|---|
8011 H18 pharmaceutical aluminium foil is a hard-temper aluminum foil substrate used for push-through pharmaceutical blister lidding for tablets, capsules and pills. It can be supplied as bare foil for downstream conversion or processed with printable primer, pharmaceutical printing and heat-seal lacquer according to the required blister packaging structure.
Typical PTP lidding foil gauges are approximately 0.020mm, 0.025mm and 0.030mm. Final thickness, width, surface condition, coating construction, reel dimensions and sealing requirements should be matched to the customer's blister packaging machine and selected forming web.
The aluminum layer provides an opaque metallic barrier, while finished blister performance also depends on pinhole control, coating integrity, heat-seal lacquer, forming web, sealing temperature, pressure and dwell time. Pharmaceutical suitability should therefore be evaluated for the complete packaging construction rather than the aluminum alloy alone.
Request Pharmaceutical Foil Pricing

| Parameter | Specification / Ordering Requirement |
|---|---|
| Product | Pharmaceutical PTP Blister Lidding Aluminium Foil |
| Primary Alloy | AA8011 |
| Temper | H18 |
| Typical Bare Foil Thickness | 0.020mm / 0.025mm / 0.030mm; other agreed pharmaceutical foil gauges subject to confirmation |
| Thickness Tolerance | To be specified according to the ordered gauge, applicable foil standard and customer pharmaceutical packaging requirement |
| Width | Custom slit width according to blister machine and converting requirements; final available range subject to production confirmation |
| Surface | Bright / matte rolling surface according to ordered foil and converting construction |
| Bare Foil Supply | AA8011-H18 aluminum foil for downstream priming, printing, lacquering and pharmaceutical conversion |
| Typical Unprinted Lidding Structure | Printable primer / Aluminum foil / Heat-seal lacquer, subject to customer specification |
| Typical Printed Lidding Structure | Protective over-lacquer / Printing ink / Aluminum foil / Heat-seal lacquer, subject to customer specification |
| Heat-Seal Lacquer | Coating chemistry and coating weight to be matched to the selected blister forming web and required sealing performance |
| Compatible Blister Web | PVC, PVDC-coated PVC and other compatible pharmaceutical blister webs subject to the specified heat-seal system |
| Printing | Unprinted or custom printed according to approved artwork, ink system, registration and pharmaceutical packaging requirements |
| Core ID | To be specified according to printing, coating, slitting and blister packaging equipment |
| Reel OD / Roll Weight | To be agreed according to customer machine capacity and handling requirements |
| Surface Quality | Clean surface without unacceptable oil contamination, stains, corrosion, wrinkles, edge damage or other defects affecting conversion |
| Pinhole Requirement | To be specified according to foil gauge and pharmaceutical packaging acceptance criteria |
| Typical Application | Push-through blister lidding for tablets, capsules and pills |
| Packing | Protected export packing according to reel configuration and pharmaceutical cleanliness requirements |
For quotation, provide foil thickness, slit width, bare or converted construction, printing requirement, heat-seal lacquer specification, blister forming web, core ID, reel OD, unwind direction, required test methods, quantity and destination.
Send Your PTP Blister Foil Specification
Pharmaceutical blister aluminium foil is the metallic lidding layer used to close individual cavities containing tablets, capsules or pills in push-through blister packaging.
The final lidding material is normally more than bare aluminum. Depending on the packaging design, one side may carry printing and a protective over-lacquer while the sealing side carries a heat-seal coating compatible with the selected blister forming web.
During packaging, the lidding foil is heat sealed over filled blister cavities. The consumer later pushes the tablet or capsule through the foil to access the product.
H18 is a hard strain-hardened condition. For conventional PTP lidding, it provides a thin foil that can remain stable during printing, coating, slitting and machine feeding while still allowing the packaged tablet or capsule to rupture the lidding when pushed through the cavity.
AA8011 can be rolled to the 20-30μm range commonly used for pharmaceutical blister lidding. The exact gauge affects reel handling, converting behavior, push-through characteristics and material consumption.
A clean, controlled foil surface is important because primers, printing inks and heat-seal coatings must adhere consistently during pharmaceutical conversion.
Intact aluminum provides an opaque barrier layer against light and has very low permeability to gases and moisture. In a finished blister, package performance also depends on pinholes, forming-web barrier, coating integrity and seal quality.
Bare foil is the rolled aluminum substrate supplied to a pharmaceutical packaging converter. It does not by itself contain printing ink, protective lacquer or a heat-seal layer.
Unprinted pharmaceutical lidding can use a printable primer on one side and a heat-seal lacquer on the sealing side. This allows the pharmaceutical manufacturer or another converter to apply approved printing later.
Printed lidding can combine an outer protective coating, pharmaceutical artwork or text, the aluminum substrate and a heat-seal lacquer. Artwork, ink system and registration requirements should be defined by the buyer.
Where printed foil is supplied, an outer protective lacquer can be used to protect the printing from rubbing and handling during conversion and packaging.
The printed side can carry product identification, batch-related information, branding or other approved packaging artwork. Ink suitability should follow the applicable pharmaceutical packaging requirement.
The aluminum layer forms the metallic lidding substrate and contributes opacity, mechanical support and barrier performance.
The sealing side is coated with a heat-seal lacquer selected for compatibility with the blister forming web. The lacquer, rather than bare aluminum itself, creates the heat-sealed bond.
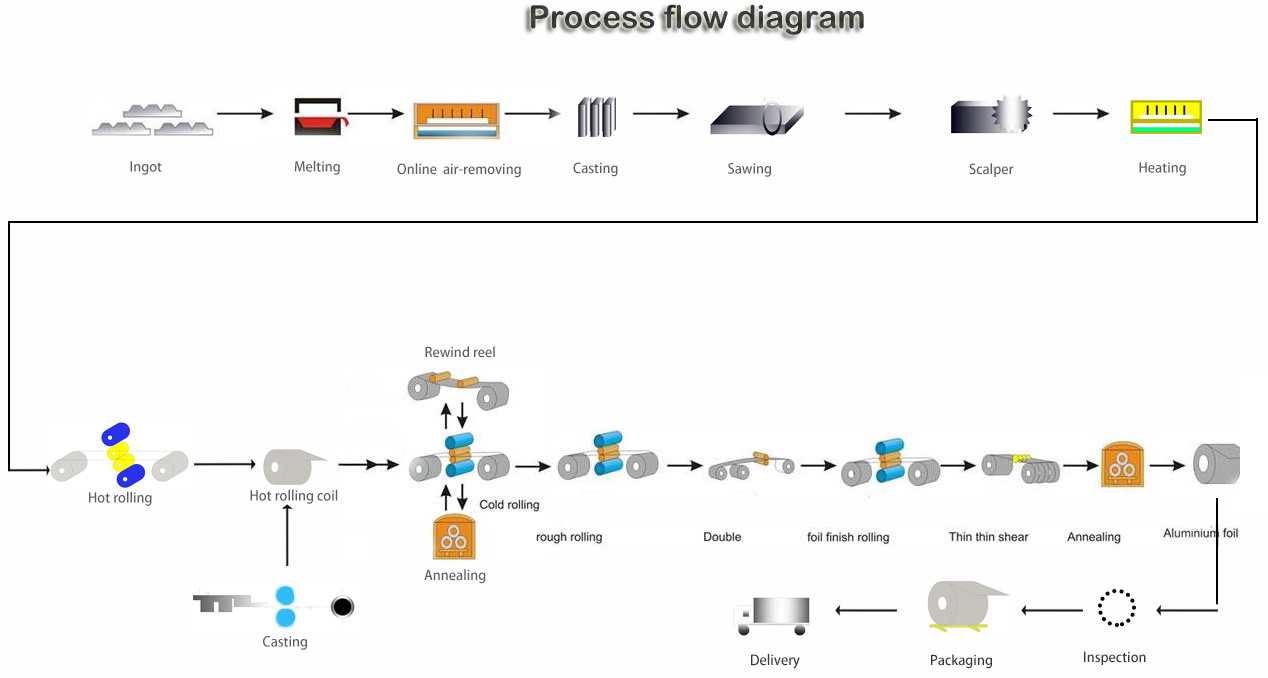
The exact mill route depends on starting stock and production equipment. A typical process for AA8011-H18 pharmaceutical foil can include aluminum stock preparation, rolling, foil rolling, surface cleaning, inspection, slitting and rewinding.
AA8011 stock is prepared through the applicable casting and rolling route before final foil reduction.
Successive rolling reductions bring the aluminum to the required pharmaceutical lidding gauge while establishing the H18 hard condition and controlling surface quality.
Rolling residues and contamination must be controlled because they can interfere with primer, printing ink or heat-seal lacquer adhesion.
The foil is slit to the required converter or blister-machine width and rewound according to the specified core, outside diameter and reel weight.
Primer, printing, protective over-lacquer and heat-seal coating can then be applied according to the required finished PTP lidding construction.
Aluminum naturally develops a thin oxide film when exposed to air. This natural oxide layer contributes to aluminum's normal surface stability, but it should not be confused with pharmaceutical primer, protective lacquer or heat-seal coating.
For pharmaceutical conversion, surface cleanliness, rolling-oil residue, wettability and coating adhesion are more important purchasing parameters than simply describing the natural oxide layer.
The opaque aluminum layer blocks light through intact areas of the lidding and can therefore contribute to protecting light-sensitive products.
Intact aluminum has very low permeability to moisture vapor and gases. Effective blister-package performance also depends on the forming web, seal integrity, coating quality and any foil defects.
Pinhole requirements should be specified for the actual foil gauge. A generic statement such as “complete barrier” should not replace contractual pinhole inspection criteria.
No fixed pharmaceutical shelf-life extension should be attributed to the aluminum foil alone. Drug-product stability depends on the formulation, forming web, lidding system, seal integrity, storage conditions and validated packaging configuration.
Bare 8011-H18 aluminum does not automatically seal to a plastic blister web. A compatible heat-seal lacquer or other specified sealing layer is required for conventional PTP blister closure.
Heat-seal lacquer should be selected for the actual forming material, such as PVC or PVDC-coated PVC. Compatibility with other pharmaceutical blister structures should be confirmed before bulk production.
Seal strength depends on temperature, pressure, dwell time, coating weight and machine condition. Buyers should provide the required sealing conditions and acceptance test where seal performance is contractual.
Uneven coating can create inconsistent sealing behavior. Coating weight and uniformity should therefore be controlled according to the approved pharmaceutical lidding specification.
Printed foil can carry approved medicine names, branding, dosage information, symbols or other packaging text according to the buyer's artwork and regulatory process.
Where text or graphics must align with individual blister cavities, registration tolerance should be agreed according to the printing and blister-machine layout.
Ink and protective coating should be selected for the finished pharmaceutical packaging construction, curing process, abrasion requirement and applicable regulatory documentation.

8011-H18 lidding foil is widely used for conventional push-through blister packages containing solid tablets.
The foil can also be used as lidding for compatible hard or soft capsule blister systems where the forming web and sealing system are appropriately specified.
Other solid oral dosage forms can use PTP lidding where the package design, cavity dimensions and validated packaging system are suitable for the drug product.
Conventional PTP lidding foil is generally a thin hard aluminum foil, commonly around 20-30μm, that seals over an already formed blister cavity and is ruptured when the dose is pushed through.
Cold-form blister material is a different product. It typically uses a softer, thicker aluminum layer such as 8021-O or 8079-O within a multilayer laminate such as OPA / Aluminum / PVC.
The cold-form laminate is mechanically formed to create the blister cavity itself. Buyers requiring Alu-Alu bottom foil should therefore provide a separate structure and forming specification rather than ordering conventional 8011-H18 lidding foil.
Pharmaceutical strip packs can also use aluminum-containing structures, but foil temper, thickness and laminate construction can differ from standard PTP lidding. Strip-pack requirements should be quoted separately.
Pharmaceutical aluminum foil is a packaging material. It does not provide pharmacological or therapeutic effects and should not be described as an active treatment for any medical condition.
Assessment should consider the complete system, including aluminum substrate, primer, printing ink, over-lacquer, heat-seal coating and the material forming the blister cavity.
Compatibility and suitability for a particular medicine should be established through the pharmaceutical manufacturer's packaging-development and stability program. The AA8011 alloy designation alone does not establish suitability for every drug.
Buyers should identify the destination market, applicable pharmacopoeial or regulatory requirements, required declarations, test reports, material certificates and change-control requirements before production.
Standard pharmaceutical blister foil should not automatically be described as sterile. If a sterile packaging component is required, sterilization method, validation and handling requirements must be defined separately.
Where AA8011-H18 is contractual, alloy and temper should be identified in the purchase specification and supported by the agreed material documentation.
The ordered 20μm, 25μm or 30μm foil should use a tolerance appropriate to pharmaceutical thin foil. A generic ±0.01mm sheet-metal tolerance is not suitable for this application.
Pinhole count or size limits can be defined according to gauge and customer acceptance criteria where barrier integrity is important.
The surface should be controlled for unacceptable rolling oil, stains, corrosion marks, scratches and contamination that could affect coating or printing.
Where primer, ink or lacquer is applied directly to aluminum, surface wettability should be controlled according to the converter's coating process and agreed test method.
Burrs, edge cracks or uneven slitting can affect reel handling and high-speed blister-machine feeding. Edge requirements should be defined where critical.
For converted foil, heat-seal lacquer and protective coating should be checked against the agreed coating-weight, adhesion and sealing requirements.
Seal-strength testing should use the specified forming web and sealing conditions. A heat-seal result obtained with one plastic structure should not automatically be applied to another.
Printed material can be evaluated for registration, legibility, color, ink adhesion, rub resistance and other approved artwork requirements.
Pharmaceutical foil reels should be protected from moisture, dust, impact, edge damage and coil deformation during handling and transport.
Packing configuration should be selected according to reel dimensions, cleanliness requirement, shipment method and the customer's handling equipment.
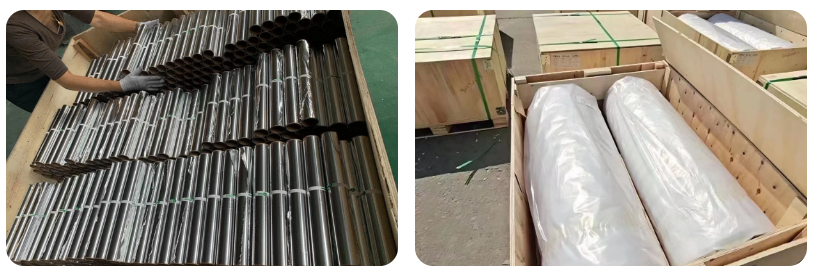
Store reels in a clean, dry indoor environment and avoid condensation or direct contact with water.
Thin foil edges can be damaged by impact. Reels should be handled with suitable lifting and support methods to prevent dents, telescoping or crushed edges.
Dust, oil and foreign particles can affect pharmaceutical printing, coating and sealing. Handling and conversion should follow the cleanliness controls required for the finished packaging component.

State whether you require bare AA8011-H18 foil or finished lidding with primer, printing, over-lacquer and heat-seal coating.
Specify the required gauge, such as 0.020mm, 0.025mm or 0.030mm, together with dimensional tolerance.
Provide the exact reel width required by the printing, coating or blister packaging line.
Identify PVC, PVDC-coated PVC or another blister material so the heat-seal coating can be matched to the actual substrate.
Provide heat-seal lacquer specification, coating weight if defined, sealing temperature range and required seal-strength test.
For printed foil, provide approved artwork, colors, print repeat, registration requirement and any variable or batch-printing arrangement.
Provide required pinhole limit, wettability, surface cleanliness, edge quality, coating adhesion and any other contractual acceptance criteria.
Specify core ID, maximum roll OD, target reel weight and unwind direction according to your equipment.
Identify the destination market and required material certificates, declarations, pharmacopoeial testing, migration or extractables requirements, change-control documentation or customer specifications.
Provide trial quantity or production quantity for each specification together with packing requirements and delivery destination.
Send Your Pharmaceutical Packaging Requirements
AA8011-H18 is commonly used as the aluminum substrate for PTP push-through blister lidding for tablets, capsules and pills.
Typical lidding gauges include approximately 20μm, 25μm and 30μm. Final thickness should follow the blister-machine, package-performance and customer specification.
Conventional 8011-H18 pharmaceutical lidding foil is more commonly specified around 0.020-0.030mm. Ultra-thin gauges can belong to other packaging applications and should not automatically be treated as standard PTP lidding foil.
H18 provides a hard foil condition suitable for conventional push-through lidding and stable downstream conversion. It is different from the soft O temper used for many cold-form applications.
No. PTP lidding foil and cold-form blister foil perform different functions. Cold-form bottom webs typically use a thicker soft aluminum layer such as 8021-O or 8079-O within an OPA/Al/PVC laminate.
Not in a conventional PTP system. A compatible heat-seal lacquer is normally applied to the aluminum so the lidding can bond to the blister forming web.
Yes. Converted lidding foil can be printed according to approved artwork, ink, registration and pharmaceutical packaging requirements.
No. Pharmaceutical aluminum foil is a packaging material and should not be described as treating ulcers, infections or other medical conditions.
AA8011 is an aluminum alloy rather than pure aluminum. The exact chemical composition should follow the applicable alloy specification.
No. Standard pharmaceutical packaging foil should not automatically be described as sterile. Sterility requires a defined and validated sterilization and handling process where the application demands it.
No. Alloy designation alone does not establish regulatory compliance. The complete packaging structure, coatings, inks, manufacturing controls and required test documentation must meet the applicable market and customer requirements.
Barrier performance depends on the aluminum lidding, forming web, pinhole condition, coating integrity and seal quality. Drug shelf life should be established from the validated complete packaging system.
Pinholes are local discontinuities in the aluminum layer. Where barrier integrity is critical, the buyer should specify permitted pinhole number or size according to the foil gauge and packaging requirement.
Rolling oil, contamination or surface defects can interfere with primer, ink and heat-seal coating adhesion. Pharmaceutical converting therefore requires controlled surface condition.
Not necessarily. Heat-seal chemistry and sealing conditions should be matched to the actual PVC, PVDC-coated PVC or other forming web used in the package.
A used pharmaceutical blister lidding component is not intended for repeated packaging use. Reuse should not be confused with material recycling.
Aluminum itself is recyclable. Actual recovery of used blister packaging depends on coatings, forming web, product contamination, material separation and the recycling infrastructure available in the destination market.
Please provide foil thickness, width, bare or converted lidding structure, blister forming web, heat-seal coating requirement, printing artwork, pinhole and surface requirements, core ID, roll OD, unwind direction, regulatory documentation, quantity and destination.
If you are sourcing AA8011-H18 aluminum foil for tablet or capsule PTP blister packaging, send us your gauge, slit width, lidding structure, forming web, heat-seal requirements, reel dimensions and pharmaceutical packaging specifications for technical confirmation and quotation.

