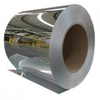
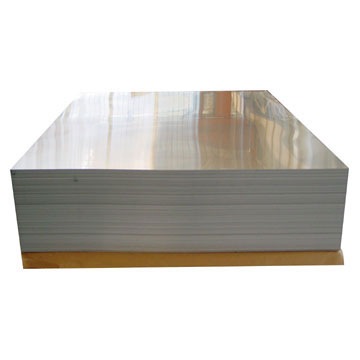
anodized aluminum coil
DINGANG
7606125000
| Availability: | |
|---|---|
| Quantity: | |
5052 anodized mirror aluminum coil combines the higher strength and corrosion resistance of an Al-Mg alloy with a bright, mirror-like anodized surface for architectural decoration, interior panels, signage, equipment housings, decorative trim and other fabricated components.
The available thickness range is 0.17-1.0mm, with listed widths of 1000mm, 1200mm and 1250mm. The material is supplied in coil form for downstream slitting, cutting, stamping, bending and fabrication according to the finished component design.
The term mirror describes the bright reflective appearance of the surface. Where a project requires a specific total reflectance, specular reflectance, diffuse reflectance or optical efficiency, the required numerical value and test method should be stated separately with the inquiry.
Custom anodized colors can be discussed according to the required appearance and production process. Because alloy composition, surface preparation, anodic film thickness, coloring and sealing can affect the final appearance, physical sample approval is recommended for visible decorative projects.
Request 5052 Mirror Aluminum Coil Pricing
| Parameter | Specification |
|---|---|
| Product | Anodized Mirror Aluminum Coil |
| Alloy | AA5052 |
| Thickness | 0.17-1.0mm |
| Width | 1000mm / 1200mm / 1250mm |
| Surface Appearance | Bright / mirror-like anodized reflective finish |
| Colors | Custom anodized colors subject to process capability, alloy response and approved appearance sample |
| Temper | To be confirmed according to forming and mechanical requirements; common 5052 flat-product conditions include O, H32, H34 and other applicable tempers |
| Tensile Strength Reference | 130MPa listed in the original specification as a reference value; final contractual value must be confirmed according to actual temper, thickness and applicable material standard |
| Yield Strength Reference | 115MPa listed in the original specification as a reference value; final contractual value must be confirmed according to actual temper, thickness and applicable material standard |
| Reflective Performance | Mirror-like visual appearance; numerical total or specular reflectance should be specified separately when required |
| Anodic Coating | Anodic film thickness and sealing requirements should be specified according to the intended application |
| Packing | Export standard wooden pallets; customized packing can be discussed |
| MOQ | 1 ton according to specification |
| Delivery Time | Approximately 25 days after receipt of the agreed deposit or L/C, subject to final specification and production schedule |
| Payment Terms | 30% T/T deposit with 70% balance against B/L copy, or 100% irrevocable L/C at sight according to agreed commercial terms |
| Typical Applications | Architectural decoration, interior panels, signage, equipment housings, elevator panels, appliance trim, decorative automotive components and suitable marine decorative components |
For an accurate quotation, provide thickness, width, temper, mirror appearance, color, required anodic coating thickness, sealing requirement, reflectance requirement if applicable, fabrication process, coil weight, quantity and delivery destination.
Send Your Coil & Surface Specification
5052 anodized mirror aluminum coil uses an Al-Mg alloy substrate that is prepared to achieve a bright decorative surface and then anodized to form an integral aluminum oxide layer.
Anodizing is an electrochemical conversion process rather than an applied paint film. The oxide grows from the aluminum surface and can subsequently be colored and sealed according to the required appearance and service conditions.
The final mirror appearance depends strongly on the surface condition before anodizing. Mechanical polishing, brightening and careful surface preparation are therefore important where high visual brightness and low visible surface distortion are required.
5052 is an aluminum-magnesium alloy that generally offers greater mechanical strength than high-purity 1xxx-series aluminum. This can be useful for decorative components that require additional rigidity after forming.
5052 is commonly selected for applications requiring good corrosion resistance. An appropriately specified anodic coating can provide additional surface protection and a controlled decorative finish.
Suitable 5052 tempers can be cut, bent, stamped and formed into decorative components. The correct temper should be selected according to bend radius, sheet thickness and required finished rigidity.
5052 can be anodized, but its final color and brightness are influenced by its alloying elements. It should not automatically be assumed to produce the same optical brightness or natural anodized tone as a high-purity bright-anodizing alloy.
Mirror appearance, gloss and optical reflectance should be treated as separate purchasing characteristics. A visually bright anodized coil may be suitable for decorative use without meeting the requirements of an engineered lighting reflector.
Total reflectance measures all light reflected from the material. Where total reflectance is a functional requirement, specify the wavelength range, instrument and minimum acceptable value.
Specular reflectance describes directional, mirror-like reflection and is more closely related to image clarity and controlled optical reflection.
Diffuse reflectance describes scattered light. Lighting, optical and display applications may therefore require both total and diffuse or specular limits.
Where maximum optical reflectivity is the primary requirement, high-purity aluminum or a specialized reflective surface may need to be evaluated instead of selecting 5052 solely for its mirror-like appearance.
The exact manufacturing route depends on the required brightness, color and anodic coating specification. A typical bright decorative anodizing process can include the following stages.
Incoming coil surface quality is important because scratches, pits and roll marks can remain visible after brightening and anodizing.
Mechanical polishing can reduce surface roughness and develop the required mirror-like appearance before chemical treatment.
Oil and processing contamination are removed before anodizing because surface cleanliness strongly affects visual consistency.
Chemical or electrochemical brightening can be used before anodizing to increase surface brightness and specularity. Brightening cannot completely remove deep scratches or major surface defects, so raw-material surface quality remains important.
The aluminum surface is electrochemically converted into a porous anodic oxide layer. Required anodic coating thickness should be specified according to appearance, fabrication and environmental requirements.
Where a colored anodized mirror surface is required, an appropriate coloring process can be applied before sealing.
Sealing reduces the porosity and absorption capacity of the anodic coating. Sealing quality should be specified where staining resistance, appearance retention or environmental durability is important.
Finished coil should be inspected for brightness, color, surface consistency and visible defects before packing. Protective film or other surface protection can be specified where required for downstream handling.
Anodic coating thickness should be specified according to the final application. A decorative interior component and an exterior architectural component may require different coating specifications.
Proper sealing is important for reducing porosity after anodizing. Where sealing performance is contractual, the applicable test method and acceptance criteria should be stated with the order.
Mirror brightness, natural anodized tone, colored finish and acceptable visual variation should be agreed using an approved sample where possible.
Where ISO 7599, AAMA 611 or another anodizing specification is required, identify the applicable coating thickness, sealing, appearance and test requirements before production.
The natural bright finish retains a metallic aluminum appearance. The exact tone depends on AA5052 chemistry, pretreatment, surface brightness and anodic coating thickness.
Custom colored finishes can be discussed according to process capability. The phrase custom color does not mean that every conventional paint color can be reproduced exactly by anodizing.
For visible architectural and decorative applications, a physical master sample is recommended for approval of brightness, color and overall appearance before bulk production.
Where adjacent components must visually match, material from coordinated production lots can help reduce visible variation. Acceptance criteria should be established before production for critical appearance projects.
Coil can be slit into narrower widths for compatible downstream components. Required width tolerance, edge condition and coil winding should be specified when automatic equipment is used.
Suitable cutting and blanking methods should minimize scratches, edge deformation and visible surface damage.
Anodic oxide is harder and less ductile than the underlying aluminum. Tight bending after anodizing can produce visible crazing or cracking at the bend. Bend radius, temper, gauge and anodic film should therefore be evaluated together.
Mild forming can be compatible with pre-anodized coil, while severe drawing or complex forming may require evaluation of whether fabrication should be completed before final anodizing.
A bright mirror surface shows scratches and handling marks more readily than a matte finish. Clean tooling, careful handling and suitable protective film should be considered during downstream fabrication.
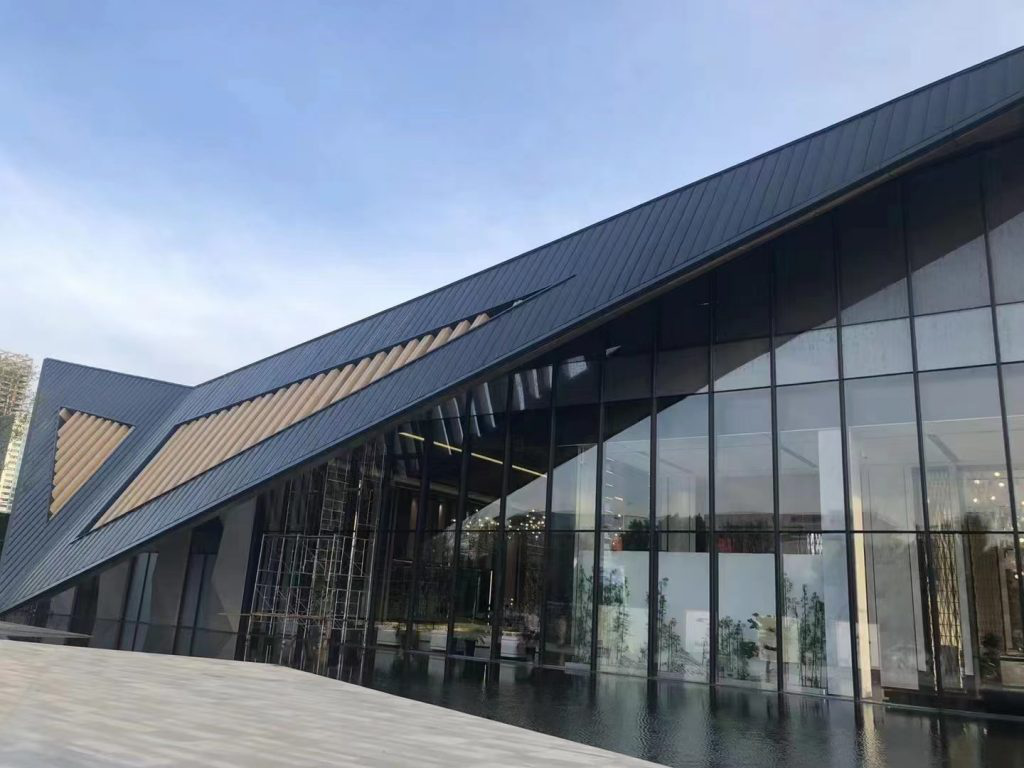
Bright anodized 5052 coil can be fabricated into suitable wall panels, ceiling components, partitions, column covers, elevator interiors and decorative trim.
The material can be evaluated for exterior decorative components where anodic coating thickness, sealing, fixing, cut edges, environmental exposure and project requirements are properly specified.
The mirror-like surface can provide a distinctive metallic appearance for suitable signs, nameplates, display stands and retail display components.
5052 anodized coil can be considered for industrial housings, instrument panels and decorative equipment covers where gauge and mechanical properties meet the component requirements.
Suitable material can be used for decorative appliance and electronics panels, bezels and exterior trim where the required forming and cosmetic specifications are satisfied.
Decorative automotive components can be evaluated where the finish, forming process, corrosion resistance and vehicle-specific validation requirements are suitable. Safety-critical components require separate engineering qualification.
5052 is widely associated with corrosion-resistant fabricated applications, but anodized mirror coil intended for marine service should still be specified for the actual salt exposure, sealing, fastening and maintenance conditions.
Decorative lighting components can use bright anodized aluminum where visual reflection is sufficient. Precision LED reflectors, optical systems, solar reflectors and other performance-critical applications should specify measured optical properties rather than rely on the term mirror aluminum.
An appropriately specified anodic coating can improve surface corrosion resistance, but aluminum can still be affected by aggressive chemicals, salt accumulation, damaged areas, unsuitable cleaners or galvanic contact.
For coastal applications, specify anodic coating thickness, sealing requirements, cut-edge design, fastener material and cleaning or maintenance conditions. The 5052 alloy name alone does not establish the service life of an anodized finished component.
Where aluminum contacts dissimilar metals in the presence of moisture, suitable isolation and fastener selection should be considered to reduce galvanic-corrosion risk.
Avoid abrasive cleaning methods and strongly aggressive chemicals on visible mirror-anodized surfaces unless their compatibility with the specified anodic finish has been established.
If AA5052 and a particular temper are contractual, identify them in the purchase specification and require applicable material documentation.
Nominal thickness, width and dimensional tolerance should be agreed according to the downstream slitting, forming and fabrication process.
If tensile strength, yield strength or elongation is contractual, provide the required temper and applicable material standard. Mechanical-property values should not be transferred between O, H32, H34 and other tempers.
Visible material should be evaluated for unacceptable scratches, dents, pits, roll marks, polishing defects, stains and inconsistent brightness under agreed inspection conditions.
Where reflectance is important, specify whether total, specular or diffuse reflectance is required together with wavelength range, test method and acceptance value.
Specify the required anodic coating thickness and measurement method rather than relying only on the description anodized aluminum.
Where sealing quality is contractual, identify the applicable test and acceptance criteria for the finished anodic coating.
Specify the required thickness from 0.17-1.0mm and the required coil width of 1000mm, 1200mm or 1250mm.
Specify O, H32, H34 or another applicable temper where mechanical properties or fabrication behavior are important.
Provide an approved surface reference where brightness, image clarity or visual appearance is important.
If the material performs a functional reflective role, provide minimum total or specular reflectance and the required measurement method.
State the required anodic film thickness and sealing requirement according to the final application.
For colored anodized material, provide an approved color or physical appearance reference.
Identify slitting, cutting, stamping, bending or other processes so the temper and surface requirements can be reviewed against the finished component.
Provide required coil quantity, preferred coil weight or packing requirements and destination. The listed MOQ is 1 ton according to specification.
Send Your Mirror Coil Specification
It is AA5052 aluminum coil with a bright mirror-like surface and an electrochemically formed anodic oxide finish for decorative and protective applications.
No. 5052 provides useful strength, formability and corrosion resistance, but higher-purity aluminum grades are generally preferred when maximum optical reflectivity is the primary requirement.
No fixed reflectance should be assumed from the term mirror aluminum. If reflectivity is contractual, specify the required total or specular value and test method.
The listed thickness range is 0.17-1.0mm.
The listed widths are 1000mm, 1200mm and 1250mm.
These are legacy reference values in the listed specification. AA5052 mechanical properties vary substantially with temper and thickness, so contractual values should be confirmed against the ordered temper and applicable material standard.
Temper should be selected according to required strength and fabrication. O temper provides greater ductility, while H32 and H34 provide higher strength with reduced forming allowance.
No. Anodizing can increase surface hardness, but abrasive contact and improper handling can still scratch or damage a bright anodized surface.
No. Proper anodizing and sealing can improve surface corrosion resistance, but aggressive chemicals, salt accumulation, damaged areas and galvanic contact can still affect the material.
5052 can be considered for suitable marine decorative applications, but the anodic coating, sealing, fasteners, salt exposure and maintenance conditions should be specified for the finished component.
Custom anodized colors can be discussed according to process capability. A physical appearance sample is recommended where color matching is important.
Moderate bending can be possible, but tight bends can visibly affect or crack the anodic layer. Temper, thickness, bend radius and anodic-film requirements should be evaluated together.
It can be evaluated for decorative lighting components, but a performance-critical LED reflector should specify measured reflectance and diffusion requirements. The mirror description alone does not establish optical efficiency.
There is no universal 10-year or 20-year service life for every anodized coil. Durability depends on anodic film thickness, sealing, environment, chemicals, cleaning, fabrication and service conditions.
Color stability depends on the coloring method, anodic coating, sealing and exposure conditions. Outdoor color-retention requirements should be specified for the actual finish.
The listed minimum order quantity is 1 ton according to specification.
The listed delivery period is approximately 25 days after receipt of the agreed deposit or L/C, subject to specification and production schedule.
Please provide thickness, width, temper, coil weight, mirror appearance, color, anodic film requirement, sealing requirement, measured reflectance if applicable, downstream fabrication process, quantity, packing requirement and destination.
If you are sourcing 5052 anodized mirror aluminum coil for architectural decoration, signage, equipment panels, elevator interiors, appliance trim or other fabricated components, send us your dimensions, temper, surface requirements, anodizing specification and quantity for technical confirmation and quotation.
Products
Application
Quick links
Contact Us