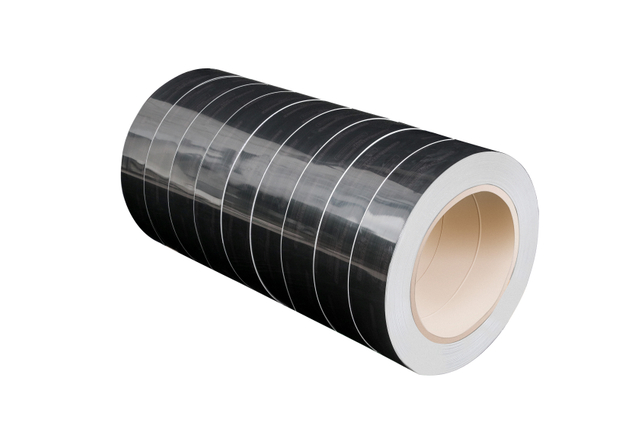
High Glossy Aluminum Coil
Dingang
7606125000
| Availability: | |
|---|---|
| Quantity: | |
AA3003 high-gloss pre-painted aluminum coil in a nominal 1.5mm thickness and 900mm width is designed as a formable decorative metal substrate for automotive trim, garnish panels, interior decorative components and suitable non-structural exterior vehicle parts.
AA3003 is a non-heat-treatable aluminum-manganese alloy offering good formability, useful corrosion resistance and moderate strength. These characteristics make it suitable for components that require cutting, slitting, bending, roll forming or stamping before assembly.
The featured product uses a 1.5mm aluminum substrate and 900mm master-coil width. The current listed production range covers 0.1-2.0mm thickness and 800-2200mm width, allowing the master coil to be slit or cut according to the finished trim dimensions and fabrication process.
PE polyester and PVDF fluorocarbon coating options are listed for this product. For automotive projects, the selected coating must be evaluated against the actual interior or exterior environment, forming requirements, scratch exposure, UV exposure, road contamination, cleaning chemicals and customer-specific performance requirements.
Request Automotive Trim Coil Pricing
| Item | Specification |
|---|---|
| Product | AA3003 High-Gloss Pre-Painted Aluminum Coil for Automotive Decorative Trim |
| Featured Size | 1.5mm thickness × 900mm master-coil width |
| Alloy | AA3003 |
| Custom Thickness Range | 0.1mm-2.0mm |
| Custom Width Range | 800mm-2200mm master-coil width |
| Temper Options | O / H12 / H14 / H16 / H18 / H24 / H26 / H32 / H34, subject to thickness, forming process and final component requirements |
| Surface Finish | High-gloss pre-painted finish |
| Coating Options | PE polyester / PVDF fluorocarbon according to project requirements |
| PVDF Coating Thickness | Current listed specification: not less than 25μm |
| PE Coating Thickness | Current listed specification: not less than 18μm |
| T-Bend | Current listed target: no more than 2T; test method and acceptance condition should be agreed where contractual |
| Color | RAL / Pantone / Approved physical color sample subject to coating availability |
| Protective Film | Temporary protective film can be specified where required for high-gloss surface protection |
| Typical Applications | Interior decorative trim, garnish panels, trim covers, decorative inserts, equipment panels and suitable non-structural exterior trim components |
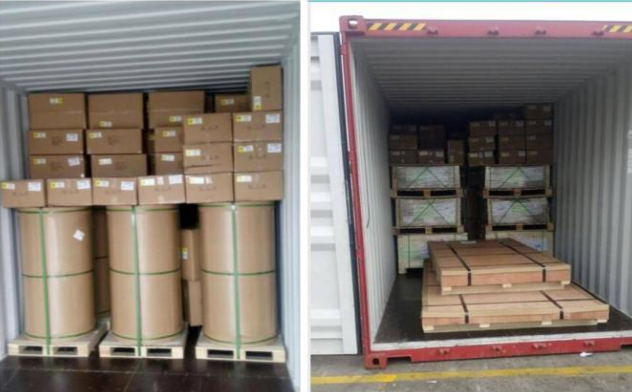
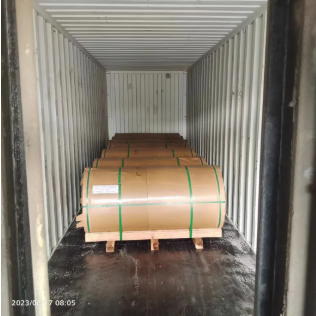
| Packing | Export-standard wooden pallets; eye-to-wall or eye-to-sky arrangement |
| MOQ | 2 metric tons per specification |
| Payment Terms | L/C at sight or 30% T/T deposit with 70% balance against B/L copy, subject to commercial confirmation |
| Typical Delivery Time | 30-45 days according to the current product information; final schedule depends on color, coating, size, quantity and production plan |
| Loading Ports | Shanghai / Ningbo / Qingdao / Tianjin or another agreed loading port |
For automotive decorative components, provide the finished-part drawing, required slit width, alloy temper, forming radius, coating type, coating thickness, gloss, color, indoor or outdoor location, protective film requirement and applicable customer test specification.
Send Your Automotive Trim Specification
AA3003 offers good forming characteristics and can be processed by bending, roll forming, pressing and other compatible fabrication methods when the selected temper and thickness match the finished geometry.
The aluminum-manganese substrate provides useful atmospheric corrosion resistance. For exterior automotive use, the complete durability system also depends on pretreatment, coating chemistry, film thickness, cut edges, forming damage and service exposure.
Aluminum has substantially lower density than conventional steel, which can reduce the mass of decorative components. Direct percentage weight-saving claims should be calculated from the actual geometry, gauge and competing material rather than assumed for every trim part.
Pre-painting provides the color and gloss before component fabrication, which can reduce the need for secondary decorative painting after the trim profile is formed.
High-gloss pre-painted AA3003 and bright anodized automotive aluminum are different product families and should not be treated as interchangeable.
The visible appearance is primarily created by the applied paint coating. This approach offers broad color flexibility and can produce black, white, solid, metallic or other decorative finishes according to the coating system.
Bright automotive trim typically relies on alloy and surface quality designed for polishing or bright anodizing. High-purity aluminum and selected aluminum-magnesium alloys are commonly considered where a metallic chrome-like or highly reflective anodized appearance is required.
A high-gloss painted surface can look smooth and reflective, but it should not automatically be described as equivalent to polished metal, bright anodized trim or electroplated chrome. If a chrome-like metallic appearance is required, provide a physical appearance standard or approved master sample.
The featured 1.5mm gauge is relatively substantial for decorative sheet and can be considered for formed garnish panels, covers and larger trim components where additional rigidity is useful.
A thicker substrate can increase local stiffness compared with thinner decorative strip, but finished-part rigidity also depends on alloy temper, ribs, folds, curvature, mounting points and component dimensions.
Increasing substrate thickness also increases forming force and minimum practical bend radius. Buyers should provide the finished trim profile where tight bends or deep forming are required.
This product is positioned as decorative pre-painted trim stock. It should not automatically be specified for crash structures, suspension components, structural battery enclosures or other safety-critical vehicle parts without a separate engineering material specification.
The featured 900mm dimension represents the master-coil width. Most finished automotive trim components are considerably narrower, so the master coil can be slit into application-specific strips according to the required developed width.
Provide the exact finished slit width and tolerance according to the roll-forming, stamping or trim-production equipment.
Edge burr, camber and slit quality should be controlled for decorative strip that feeds continuously through forming equipment.
Where processing equipment has specific limits, provide the required inner diameter, maximum outside diameter, coil weight and winding direction with the inquiry.
Pre-painted AA3003 can be evaluated for suitable interior garnish panels, decorative inserts, console trim, instrument-panel accents and other non-structural visible metal components.
Suitable slit and formed aluminum can be evaluated for decorative door or window-area garnish where the selected coating meets forming, exterior exposure and appearance requirements.
Formed pre-painted aluminum can be considered for suitable decorative covers and trim pieces around roof, pillar or upper-body areas when attachment, wind exposure and coating durability have been validated.
The material can also be evaluated for non-structural exterior or interior decorative panels on trucks, trailers, buses and specialty vehicles where the coating specification matches the expected service environment.
Custom colors and high-gloss finishes can support aftermarket decorative products when the component design, forming process, mounting system and environmental requirements are clearly defined.
| Requirement | Interior Trim | Exterior Trim |
|---|---|---|
| UV Exposure | Primarily through vehicle glazing and interior light exposure | Direct sunlight and weather exposure can require stronger weathering performance |
| Scratch Exposure | Handling, cleaning and occupant contact | Road debris, washing, handling and environmental contamination |
| Chemical Exposure | Interior cleaners, skin oils and household-type contaminants | Road salt, detergents, car-wash chemicals, fuel or other exterior contaminants depending on location |
| Temperature Cycling | Cabin temperature cycles according to vehicle environment | Direct environmental temperature cycling and solar heating |
| Coating Selection | Based on appearance, scratch resistance, chemical resistance and interior customer requirements | Based on weathering, corrosion, chip resistance, chemical resistance, color retention and customer-specific exterior requirements |
PE polyester coating can provide a high-gloss decorative finish with broad color flexibility. The current product specification lists a PE coating thickness of not less than 18μm.
For automotive use, the specific polyester coating should be evaluated for forming, scratch resistance, chemical exposure, temperature cycling and any customer-specific durability requirements.
The current product information also lists PVDF coating with a film thickness of not less than 25μm. PVDF is known for exterior weathering capability, but a general architectural PVDF coating should not automatically be assumed to satisfy an automotive OEM exterior-trim specification.
Where PVDF is requested for vehicle components, the coating formulation, forming compatibility, adhesion and required automotive tests should be agreed for the actual component.
Where the customer has a defined vehicle or OEM specification, provide the required coating chemistry, color, gloss, film thickness, hardness, adhesion, bend performance, weathering, chemical resistance and other test criteria rather than relying only on the generic terms PE or PVDF.
“High gloss” is a general appearance description. If gloss is a contractual requirement, specify the target gloss range and applicable measurement geometry.
Automotive decorative surfaces are appearance-sensitive. A physical coated-aluminum sample should be approved for color, gloss, metallic effect and surface appearance before production where these characteristics are critical.
Where color consistency is contractual, define the required instrumental color-difference tolerance and measurement conditions rather than using an undefined “no color difference” requirement.
Metallic or effect coatings can show directional appearance. Coil direction, slitting direction, forming direction and component installation orientation should be controlled where visual matching is important.
High-gloss coated aluminum is visually sensitive to scratches, roller marks, dirt and handling damage. Protective handling should therefore be considered throughout slitting, forming, packaging, assembly and transportation.
Temporary PE protective film can be specified where required. Film adhesion, aging behavior and removal conditions should be compatible with the coating and downstream manufacturing process.
Rollers, dies, guides and worktables should be clean and free from abrasive contamination because marks that are minor on a matte surface can be highly visible on a high-gloss trim component.
Converted trim parts may require interleaving, trays, protective film or non-abrasive packaging to prevent face-to-face rubbing before vehicle assembly.
The 900mm master coil can be slit into narrower automotive trim strips. Finished strip width, burr, camber and winding requirements should be defined according to the customer's forming line.
Suitable AA3003 tempers can be roll-formed into decorative profiles. Roller geometry, forming stages and coating protection should be optimized to reduce scratching and excessive strain on the paint film.
Shallow stamped or pressed decorative parts can be evaluated according to temper, material direction, forming depth and coating elongation requirements.
Bend performance depends on temper, 1.5mm substrate thickness, bend radius, coating system and forming direction. No coating system should be promised to remain crack-free under every bend condition.
The current product specification lists T-bend of no more than 2T. Where this value is contractual, confirm the applicable test method, substrate temper, coating system and acceptance criteria before production.
Exterior trim can be exposed to prolonged sunlight and weathering. Required color and gloss retention should be specified using the customer's applicable test conditions or approved coating specification.
Road salt, water and dirt can accumulate around exterior trim. Corrosion performance depends on the substrate, pretreatment, coating, cut edges, mounting design and galvanic contact with adjacent materials.
Components positioned near wheel paths or lower body areas can require chip or impact resistance. If this is important, provide the applicable impact or gravel test requirement rather than assuming a decorative high-gloss coating provides sufficient protection.
Exterior and interior trim can be exposed to detergents, cleaners, waxes and other chemicals. Chemical compatibility should be evaluated against the actual substances and customer test requirements.
Automotive trim experiences repeated temperature changes. Coating adhesion, dimensional movement and mounting design should be evaluated for the actual environmental temperature cycle required by the vehicle program.
| Material Option | Selection Considerations |
|---|---|
| Pre-Painted AA3003 Aluminum | Lower density than steel, useful formability and broad paint-color options. Surface durability depends on pretreatment, coating and final exposure. |
| Stainless Steel Trim | Higher density and different mechanical properties, with metallic appearance available without an organic color coat. Cost and forming requirements vary by grade and component. |
| Chrome-Look Plastic | Supports complex molded geometry and low component weight. Thermal, UV, coating and mechanical performance depend on the selected polymer and decorative process. |
| Bright Anodized Aluminum | Provides a metallic anodized appearance and is commonly based on alloys selected for surface quality and anodizing response. Color and appearance differ from painted high-gloss aluminum. |
Where AA3003 and a specific temper are contractual, they should be stated on the purchase order and verified against the applicable material documentation.
The featured 1.5mm substrate and any customized thickness should be inspected against the agreed dimensional tolerance.
Both master-coil width and finished slit-strip width should be controlled where strip dimensions affect downstream forming equipment.
PE, PVDF or another agreed coating should be measured according to the specified dry-film thickness and applicable test method.
Visible automotive trim should be evaluated against the approved color and gloss standard where appearance consistency is required.
Adhesion should be tested according to the agreed coating specification, particularly where the material will be formed after painting.
T-bend or another agreed forming test can be specified to evaluate coating integrity after deformation.
High-gloss material should be inspected for agreed limits on scratches, dents, roll marks, dirt, stains, coating defects and other visible imperfections.
Where required, provide the applicable customer or vehicle-program requirements for weathering, humidity, corrosion, chip resistance, chemical resistance, temperature cycling and other durability tests before production.
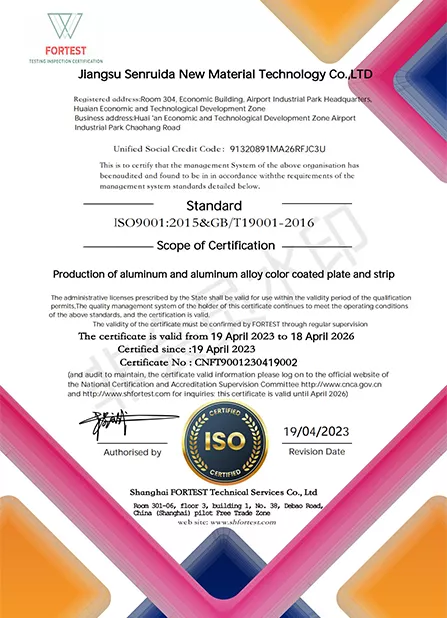
Material certificates, coating inspection reports and other supporting documents can be supplied according to the agreed order requirements. The exact document, test standard, issuing organization and product scope should be confirmed before production.
Pre-painted aluminum coils can be lined with moisture-resistant paper, wrapped with waterproof protective material and secured in seaworthy export packaging to reduce moisture exposure, edge damage and coil movement during transportation.
Eye-to-wall or eye-to-sky packing can be selected according to coil dimensions and handling requirements. Customized packaging can be discussed according to customer unloading, storage and downstream slitting requirements.
Specify AA3003 together with the required temper according to stiffness, bend radius and forming process.
The featured product is 1.5mm thick. Provide the required thickness tolerance where component fit and forming depend on gauge.
The featured master coil is 900mm wide. If narrower trim strip is required, provide the finished slit width, tolerance, camber and edge-quality requirements.
State the trim location on the vehicle because interior and exterior components can have substantially different coating and durability requirements.
Provide PE, PVDF or another customer-approved coating chemistry together with primer, topcoat and back-coat requirements where applicable.
Provide color reference, numerical gloss requirement and approved physical appearance sample where the decorative finish is critical.
Identify whether the strip will be roll-formed, bent, stamped, punched or otherwise shaped and provide minimum bend radius or finished-part drawings.
List the required adhesion, T-bend, scratch, chip, weathering, corrosion, humidity, chemical or temperature-cycle tests according to the customer specification.
Provide core ID, maximum coil OD, maximum coil weight, winding direction and protective film requirement where relevant to the production line.
Request a Custom Automotive Trim Coil Specification
It is AA3003 aluminum coil supplied with a factory-applied high-gloss decorative coating before slitting, forming or fabrication into finished components.
The featured product uses a 1.5mm aluminum substrate and a 900mm master-coil width.
The current listed thickness range is 0.1mm to 2.0mm.
The current listed master-coil width range is 800mm to 2200mm.
Yes. The 900mm dimension can serve as a master-coil width for downstream slitting. Provide the required finished strip width and tolerance for production confirmation.
There is no single temper for every trim profile. Softer conditions provide greater forming allowance, while harder conditions provide greater rigidity. Select the temper according to thickness, bend radius and finished geometry.
AA3003 can be used as a formable painted decorative substrate, but very bright anodized automotive trim commonly uses alloys selected specifically for high surface quality and anodizing response. If a metallic chrome-like finish is required, the appearance and alloy should be specified separately.
No. High-gloss paint, polished aluminum, bright anodized aluminum and electroplated chrome use different surface systems and produce different visual effects.
It can be evaluated for suitable non-structural exterior trim when the coating system meets the required weathering, corrosion, chip, chemical and temperature-cycle requirements of the application.
Yes, suitable high-gloss AA3003 can be evaluated for decorative interior panels, inserts and garnish components according to appearance, forming and customer durability requirements.
This product is positioned as decorative pre-painted material. Structural or safety-critical automotive parts require a separate engineering alloy and mechanical-performance specification.
The current product information lists PE paint coating thickness of not less than 18μm.
The current product information lists PVDF paint coating thickness of not less than 25μm.
No. PVDF describes a coating chemistry. An automotive program can require specific adhesion, weathering, chip, corrosion, chemical and temperature-cycle tests that must be verified for the actual coating system.
The current product specification lists T-bend of no more than 2T. If this value is contractual, the applicable test method, coating system, temper and acceptance condition should be agreed before production.
Forming performance depends on alloy temper, substrate thickness, coating flexibility, bend radius, material direction and tooling. Representative material should be trialed for severe bends or complex trim profiles.
No. Gloss describes appearance, not scratch resistance. High-gloss surfaces can make small scratches particularly visible, so hardness and scratch requirements should be specified separately.
Temporary protective film can be specified where required to reduce surface damage during slitting, forming, transportation and assembly.
RAL, Pantone or approved physical samples can be used as color references subject to paint-system availability and production confirmation. Automotive appearance-sensitive programs should approve a physical sample before bulk production.
The current listed MOQ is 2 metric tons per specification. Final minimum quantity can vary according to gauge, width, slit configuration, color and coating system.
The current listed production lead time is approximately 30-45 days. Final schedule depends on raw-material availability, coating, color, slitting, quantity and sample approval requirements.
Sample material or color samples can be discussed before bulk production so appearance and forming performance can be evaluated against the customer's component requirements.
Please provide AA3003 alloy requirement, temper, substrate thickness, master-coil width, finished slit width, coil ID or maximum OD, coating chemistry, dry-film thickness, color, gloss, interior or exterior location, bend radius, finished-part drawing, protective film requirement, customer test specification, quantity and delivery destination.
If you are sourcing AA3003 1.5mm × 900mm high-gloss pre-painted aluminum for automotive trim, garnish panels or other non-structural decorative vehicle components, send us your finished width, temper, coating, color, gloss, forming requirements and test specification for technical confirmation and quotation.
Products
Application
Quick links
Contact Us