AA3003
Dingang
7606125900
| Availability: | |
|---|---|
| Quantity: | |
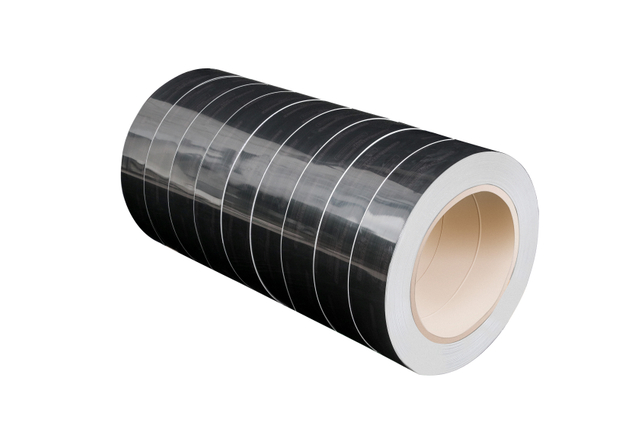
This 1.0mm O temper high gloss color coated aluminum coil is designed for warehouse roofing, industrial building roof renovation, roof cladding, canopies and architectural components requiring high formability together with a smooth decorative finish.
Available with 1060 or 3003 aluminum substrate, the fully annealed O temper provides high ductility for bending, profiling, folding and compatible roll-forming processes. PE polyester and PVDF coating systems are available according to the required exterior exposure and project performance.
The standard product is supplied at 1.0mm thickness with widths from 600mm to 1500mm. The published coating specification includes 15–25μm top coating, 5–10μm back coating and an 85–95 high-gloss range. Industrial gray, blue, white, dark green and custom colors can be discussed according to project requirements.
Item | Technical Specification |
|---|---|
Product Type | High gloss color coated / prepainted aluminum coil for warehouse roofing |
Substrate Alloy | 1060 / 3003 aluminum alloy |
Temper | O Temper, fully annealed |
Nominal Thickness | 1.0mm; other thickness requirements can be discussed |
Width Range | 600mm–1500mm; custom widths available |
Coating Type | PE polyester / PVDF |
Coating Construction | Pretreatment / primer / topcoat with reverse-side coating according to the confirmed specification |
Published Top Coating Thickness | 15–25μm |
Published Back Coating Thickness | 5–10μm |
Published Gloss | 85–95 high-gloss range |
Surface Finish | Smooth high-gloss decorative surface |
Color Options | Industrial gray, blue, white, dark green and custom approved colors |
Processing | Bending, profiling, cutting, slitting and roll forming according to project requirements |
Protective Film | Available according to fabrication and visible-surface protection requirements |
Coil ID / Coil OD | To be confirmed according to decoiler and production-line requirements |
Coil Weight | Customized according to handling and equipment limits |
Typical Applications | Warehouse roofing, factory roofs, industrial cladding, canopies, fascia, flashing and roof accessories |
Final alloy, dimensional tolerances, coating construction, gloss tolerance, color reference, coil dimensions, protective film and packing requirements should be confirmed in the purchase specification before production.
Get Technical Specifications & Pricing
O temper aluminum is fully annealed and provides greater ductility than harder H tempers. This characteristic is useful where the material must undergo substantial bending, profiling or folding.
The material can be considered for compatible warehouse roof profiles when alloy, thickness, profile geometry, forming stations, roller pressure and coating flexibility are matched to the production equipment.
O temper can also be useful for ridge caps, flashing, fascia, gutters, roof-edge components and other folded parts where forming flexibility is more important than maximum material hardness.
High formability does not by itself establish suitability for every structural roof panel. Roof profile depth, support spacing, wind loads, snow loads, fastener design and applicable building requirements should be reviewed for the complete roofing system.
Selection Factor | 1060 Aluminum | 3003 Aluminum |
|---|---|---|
Alloy Type | Commercially pure aluminum | Aluminum-manganese alloy |
Formability | High formability in suitable tempers | Useful formability with higher alloy strength |
Relative Strength | Lower than 3003 | Higher than 1060 due to manganese alloying |
Selection Consideration | Consider where high forming capability is prioritized | Consider where greater finished strength or rigidity is required |
The final alloy should be selected according to roof profile geometry, forming severity, required stiffness and project engineering requirements rather than appearance alone.
The published gloss range of 85–95 provides a bright, reflective architectural appearance for visible warehouse roofs, industrial buildings and related exterior components.
Where gloss is contract-critical, the purchase specification should state the target gloss, measurement method and acceptable tolerance. Color and gloss should be approved separately because the same nominal color can appear different at different gloss levels.
High-gloss surfaces can reveal scratches, roller marks and handling damage more readily than matte finishes. Clean tooling, controlled handling and optional protective film can therefore be important during fabrication and installation.
The current published product specification lists a 15–25μm top-coating range and a 5–10μm back-coating range.
The visible top surface provides the primary architectural color and finish, while the reverse-side coating can provide additional protection during fabrication and service.
Final film build should be confirmed according to whether PE or PVDF is selected, the installation environment, forming requirements and project acceptance criteria.
Selection Factor | PE Polyester | PVDF |
|---|---|---|
Typical Use | General warehouse roofing and architectural components | More demanding exterior roofing and architectural applications |
UV Exposure | Suitable where the selected polyester system meets project requirements | Generally selected where higher UV and long-term color-retention performance are required |
Typical Environment | General industrial and warehouse environments | High-UV, coastal or more demanding environments subject to specification review |
Cost Consideration | Economical option for suitable general roof projects | Typically selected where exterior durability is a higher priority |
Coating selection should consider UV exposure, rainfall, humidity, coastal salt, industrial pollution, roof orientation, color and expected appearance retention.
Performance Item | What to Confirm | Application Relevance |
|---|---|---|
T-Bend / Flexibility | Agreed bend requirement according to roof profile | Helps evaluate coating behavior during folding and roll forming |
Coating Adhesion | Cross-cut, tape or other agreed method | Checks bonding between coating and aluminum substrate |
Coating Cure | MEK/solvent resistance or another agreed test where specified | Useful for confirming adequate coating cure |
Surface Hardness | Pencil hardness or agreed surface requirement | Helps evaluate handling resistance of visible surfaces |
Humidity / Corrosion | Agreed test method and acceptance criteria where required | Important for humid, coastal or industrial installations |
Color Difference | Approved master sample and agreed tolerance | Important where multiple coils appear on one roof elevation |
The 85–95 high-gloss surface provides a bright decorative appearance suitable for visible warehouse roofs, industrial buildings, canopies and architectural components.
The fully annealed O temper provides high ductility for compatible bending, folding and profiling operations. Final performance should still be validated against the actual roof geometry and production equipment.
Aluminum has a relatively low density, which can simplify transportation, coil handling, fabrication and installation of compatible roofing components.
The aluminum substrate naturally forms a protective oxide layer, while the selected PE or PVDF paint system provides decorative color and additional surface protection.
Widths from 600mm to 1500mm are available within the published range. Industrial gray, blue, white, dark green and other approved colors can be discussed according to production feasibility and quantity.
1.0mm O temper high gloss coated aluminum coil can be considered for compatible industrial roofing and architectural applications including:
Warehouse roof panels
Warehouse roof renovation
Factory and workshop roofing
Logistics-building roof cladding
Industrial roofing profiles
Exterior industrial building cladding
Roof fascia and flashing
Ridge caps and roof-edge components
Storage-building canopies
Sunshade and shelter components
Discuss Your Warehouse Roofing Project
For trapezoidal, corrugated or other roll-formed roof profiles, buyers should provide the profile drawing where possible. Profile depth, rib geometry, bend radii and forming sequence affect material and coating performance.
Roller alignment, pressure, surface cleanliness and line speed can influence both profile dimensions and the visible high-gloss coating. Production equipment should be adjusted to avoid unnecessary scratching or coating damage.
For flashing, ridge caps, fascia, gutters and other folded components, the required bend radius should be considered together with aluminum temper and coating flexibility.
Where a severe or 180-degree fold is required, suitability should be confirmed on representative material. Actual performance depends on bend radius, alloy, coating system, film build and tooling rather than O temper alone.
For new roof profiles or demanding forming operations, a production-line trial is recommended before bulk ordering to verify forming, dimensions and coating integrity.
Industrial gray, blue, white and dark green are available within the published range, while additional colors can be discussed according to production requirements.
For projects requiring accurate color matching, buyers should provide an approved physical sample, RAL reference, Pantone reference or another agreed standard.
The published gloss range is 85–95. Where appearance consistency is important, the target gloss and permitted deviation should be included in the order specification.
Where multiple coils will be installed on one visible roof elevation, batch planning can help reduce visible differences in color and gloss.
Warehouse roofs can experience strong UV exposure, high surface temperatures, rainfall, condensation, industrial pollution and, in coastal areas, airborne salt.
The selected PE or PVDF system should therefore be matched to the actual installation environment rather than chosen only by color or initial gloss.
For coastal, high-UV or heavily polluted industrial environments, buyers should state the exposure conditions and required performance before the coating construction is approved.
Inspection can include aluminum thickness, coil width, coating thickness, surface appearance, color, gloss, edge condition and coil dimensions according to the agreed purchase specification.
Where forming performance is important, buyers can specify T-bend, coating adhesion or representative roll-forming requirements together with the applicable acceptance criteria.
Where coating cure or surface resistance is important, solvent resistance, pencil hardness or another agreed coating test can also be included in the inspection plan.
For visible warehouse roofs, approved color samples and gloss requirements should be retained as production references for repeat orders.
Coils can be supplied with moisture-resistant wrapping, edge protection, secure strapping and export packing according to coil dimensions and transportation requirements.
Buyers using automatic or semi-automatic roof-panel lines should specify core ID, maximum coil OD, maximum coil weight, slit width and winding requirements before production.
Eye-to-wall or eye-to-sky packing requirements can be discussed where warehouse handling, crane lifting or production-line loading requires a specific coil orientation.
To receive an accurate quotation and material review, please provide as much of the following information as possible:
Required alloy: 1060, 3003 or another specified grade
O temper requirement
Required thickness and tolerance
Required width and tolerance
PE or PVDF coating
Required topcoat thickness
Required back-coat thickness
Color or approved physical color reference
Target gloss and acceptable tolerance
Protective-film requirement
Roof profile drawing
Profile depth and bend radii
Roll-forming or bending method
Required T-bend or coating-adhesion test, if specified
Core inner diameter
Maximum coil outside diameter
Maximum or preferred coil weight
Warehouse, factory, workshop or other final application
Installation climate and environmental exposure
Order quantity or annual consumption
Eye-to-wall or eye-to-sky packing requirement
Destination country or delivery port
Special inspection or documentation requirements
Send Your Specifications for a Quote
It is 1.0mm aluminum coil in a fully annealed condition with a factory-applied color coating. This product is available with 1060 or 3003 substrate and PE or PVDF coating.
O temper means the aluminum has been fully annealed. It provides high ductility and is useful for applications requiring substantial bending, folding or profiling.
It can be used in compatible warehouse roofing systems, but suitability depends on roof profile, support spacing, wind and snow loads, fastening design and applicable project requirements.
1060 provides high formability, while 3003 generally provides greater strength because of manganese alloying. The final choice should reflect the profile geometry, forming severity and required finished rigidity.
PE is commonly used for suitable general roofing applications, while PVDF is generally considered where higher UV resistance, weathering and long-term color retention are required.
The published specification lists a 15–25μm top coating and a 5–10μm back coating. Final film build should be confirmed for the selected PE or PVDF system.
It is the published high-gloss range for this product. Where gloss is an acceptance requirement, the measurement method and permitted tolerance should be defined in the order.
Yes, for compatible profiles. Actual performance depends on alloy, profile geometry, forming stations, tooling, line settings and coating flexibility.
O temper provides high ductility, but a successful 180-degree fold cannot be assumed from temper alone. Bend radius, alloy, coating construction and tooling should be validated using representative material.
T-bend testing can help evaluate whether the coating remains suitably adhered after the aluminum is tightly folded or formed. The required acceptance level should reflect the actual roof profile.
The published width range is 600mm to 1500mm. Custom widths can be discussed according to production capability, tolerance and order quantity.
Yes. Industrial gray, blue, white and dark green are listed options, while other colors can be discussed. A physical sample or approved color reference is recommended before production.
Protective film can be discussed where additional protection is required for the high-gloss surface during roll forming, fabrication, transportation or installation.
Sample availability can be confirmed according to alloy, coating, color and gloss. For a new roof profile or forming line, representative production trials are recommended before volume ordering.
Please provide alloy, thickness, width, PE or PVDF coating, film thickness, color, gloss, coil dimensions, roof profile, forming method, environmental conditions, quantity and destination.
Products
Application
Quick links
Contact Us