PPAL
DINGANG
| Availability: | |
|---|---|
| Quantity: | |
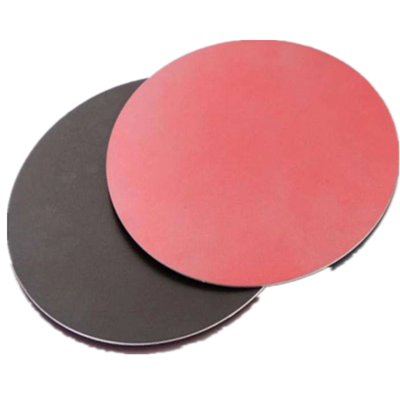
1060-O prepainted aluminum circle is a factory-coated round aluminum blank designed for cooking pots, cookware lids and selected kitchenware components that require a finished decorative or protective surface before final assembly.
AA1060 provides high aluminum content, good thermal conductivity, low density and useful formability. The O-temper substrate can be selected where greater ductility is required, while the broader prepainted aluminum circle range also includes harder tempers for applications requiring increased rigidity.
PVDF, PE and application-specific paint systems are available within the coated-circle range. Coating type, film thickness, color, gloss, forming depth and intended cookware surface should be specified before production so that the substrate and paint system can be matched to the finished component.
Request 1060-O Prepainted Circle Price
| Product | Prepainted aluminum circle / color-coated aluminum disc for cookware components |
| Primary Alloy | AA1060 |
| Primary Temper | O temper / annealed condition |
| Available Alloy Range | 1050, 1060, 1100, 3003, 3005, 3105 |
| Other Prepainted Temper Options | H14, H18, H24 and other application-specific conditions subject to confirmation |
| Listed Diameter Range | 100–800 mm; common diameters include 300, 400, 500, 600 and 800 mm |
| Listed Punching Thickness | Up to 1.20 mm; other thickness and cutting requirements should be confirmed before ordering |
| Coating Options | PVDF, PE and application-specific coating systems |
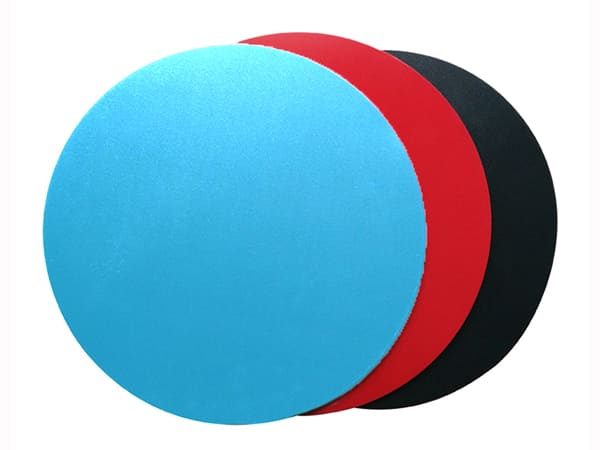
| Color | Custom colors according to buyer specification or approved physical sample |
| Forming | Punching, stamping and selected forming operations subject to coating flexibility, temper and finished-part geometry |
| Typical Applications | Cooking-pot components, cookware lids, covers, shallow-formed kitchenware, appliance components and other prefinished round parts |
| MOQ | 1,000 kg per size according to the listed product information |
| Lead Time | Within approximately 30 days, subject to coating, color, size and order quantity |
| Payment | T/T or irrevocable L/C at sight |
| Sample | Sample pieces can be discussed for color, coating and forming evaluation before bulk production |
A prepainted aluminum circle already carries the specified decorative or protective coating before it reaches the cookware production line. For compatible components, this can reduce or eliminate a separate post-forming painting operation.
Industrial coil coating provides controlled film application over the aluminum substrate. Color, gloss and film thickness can be specified before circular blanks are produced, supporting consistent appearance across production batches.
AA1060 has relatively low density compared with many other metallic materials, helping manufacturers produce lightweight cookware and appliance components.
The high aluminum content of AA1060 provides good thermal conductivity, making it a practical substrate for suitable cookware parts where heat transfer is required.
Different colors and coating constructions can be discussed according to the finished product. Buyers should provide the intended application, color reference, coating side and performance requirements when requesting a quotation.
The following values summarize the listed coating-performance range for the existing prepainted aluminum circle product family. The exact coating construction and acceptance criteria should be confirmed before production because forming requirements and end-use conditions differ between cookware components.
| Test Item | Paint System | ||
| PVDF | PE and Others | ||
| With Varnish | Without Varnish | ||
| Paint Film Thickness | ≥22 µm | ≥30 µm | ≥18 µm |
| Gloss / Shine Tolerance | Shine ≥80 units: ±10 units allowed; Shine 20–80 units: ±7 units allowed; Shine <20 units: ±5 units allowed | ||
| Pencil Hardness | ≥1H | ||
| Abrasion Resistance | ≥5 L/µm | — | |
| T-Bend | ≤2T | ≤3T | |
| Impact Strength | 50 kg·cm without coating loss or cracking according to the listed requirement | ||
| Adhesion Class | ≥1 | ||
| Boiling Water Resistance | Listed result: unchanged | ||
| Acid Resistance | Listed result: unchanged | ||
| Alkali Resistance | Listed result: unchanged | ||
| Oil Resistance | Listed result: unchanged | ||
| Solvent Resistance | ≥70 | ≥50 | |
| Scrub Resistance | ≥10,000 cycles with no listed change | ||
| Dirt Resistance | ≤15% | — | |
| Salt Spray Resistance | ≥2 class | — | |
PVDF coating is available within the wider prepainted-circle range when higher coating durability, chemical resistance or application-specific performance is required. For cookware, suitability depends on which side of the component is coated and the actual service conditions.
PE and other application-specific coating systems can be selected for decorative surfaces and suitable cookware components. Required film thickness, gloss, color and forming behavior should be defined according to the finished part.
Discuss Your Coating and Color Requirements
A coated aluminum circle behaves differently from an uncoated mill-finish blank during forming. The aluminum substrate may have sufficient ductility, but the paint film must also tolerate stretching and bending without unacceptable cracking, whitening or loss of adhesion.
For shallow stamping, lids and compatible formed components, a flexible coating system can be evaluated against the required bend radius and deformation. T-bend, impact and adhesion results provide useful references, but they do not replace an actual production trial.
For severe deep drawing of high-wall cooking pots or pans, forming a mill-finish circle first and applying the final cookware coating afterward may be more suitable. If a prepainted blank must be deeply formed, the complete substrate-and-coating system should be qualified using the customer's actual tooling and draw depth.
The listed PVDF and PE coating-performance values describe the available prepainted product range and do not by themselves establish suitability for direct food contact.
If the coated surface will directly contact food, the cookware manufacturer should specify the required food-contact coating system, intended cooking temperature, destination-market requirements and any required test documentation before production.
For decorative exterior surfaces, cookware lids or other non-food-contact areas, coating selection should be based on the required appearance, forming performance, cleaning resistance and service environment.
Cooking-pot exterior components
Cookware lids and covers
Shallow-stamped cookware components
Electric cooker and appliance covers
Decorative kitchenware parts
Prefinished round appliance components
Application-specific cookware parts using a validated coating system
Continuous roller coating allows the paint film to be applied under controlled production conditions before the circular blanks are produced. This supports more consistent film thickness and surface appearance across a production batch.
Factory coating can provide uniform color and gloss for cookware programs where multiple components need to maintain a consistent decorative appearance.
When the coating has been validated for the required forming operation, manufacturers can use prefinished blanks and reduce later painting and curing steps for suitable components.
Prepainted aluminum circles are produced from coated aluminum material and converted into round blanks according to the required diameter. Production control should include surface appearance, coating condition, color, gloss, diameter, thickness and circle edge quality.


Verify circle diameter, thickness and dimensional tolerance against the approved cookware or component drawing before loading material into production.
Check for scratches, dents, coating holidays, contamination, color variation and other visible defects that could remain on the finished component.
Circle edges should be sufficiently clean for safe handling and the intended forming operation. Excessive burrs or edge damage may affect stamping or become initiation points for cracking.
For a new coating system, thickness or cookware profile, a trial using the actual production tooling is recommended to check coating adhesion, cracking, whitening and finished surface appearance.
For branded cookware or repeat orders, compare supplied material against the approved color and gloss reference before bulk forming.
Specify whether the circle will be used for a pot component, lid, cover, shallow-formed part or another finished product. The component geometry determines the required forming severity.
The listed diameter range is approximately 100–800 mm. The listed punching capability is up to 1.20 mm thickness. Other thickness-and-diameter combinations should be reviewed before ordering.
O temper provides greater substrate ductility, while harder tempers can provide greater rigidity. Temper selection should be matched to the amount of stamping or forming required after coating.
Specify PVDF, PE or another approved coating construction together with the required film thickness, coating side, color, gloss and performance requirements.
Provide the intended stamping depth, bend radius or finished drawing. Greater deformation places higher demands on both the aluminum substrate and the paint film.
If the coated side will directly contact food, specify the required destination-market and food-contact requirements before coating selection and sample approval.
For a faster and more accurate quotation, please provide:
Required aluminum alloy
Temper
Circle diameter
Thickness
Dimensional tolerances
PVDF, PE or other coating type
Required coating thickness
Color and gloss reference
Coated side or sides
Finished cookware component
Stamping or forming depth
Food-contact requirement, if applicable
Required quantity per size
Destination port or delivery location
For a new coated cookware component, providing the finished-part drawing and forming sequence can help determine whether the requested coating is suitable for the required deformation.
Send Your Prepainted Circle Requirements
It is an AA1060 aluminum circular blank with a factory-applied coating and an annealed substrate condition. It can be used for suitable cookware, lid and appliance components where a prefinished surface is required.
They can be used for suitable pot components, lids and selected formed cookware parts. The coating system and forming process must be matched to the actual component and service conditions.
Forming capability depends on substrate temper, paint flexibility, film thickness, blank thickness, drawing depth and tooling. Shallow forming may be practical with a suitable coating, while severe deep drawing requires specific validation.
The listed range is approximately 100–800 mm, including common diameters such as 300, 400, 500, 600 and 800 mm. Other requirements can be discussed according to production capability.
The existing product information lists punching capability up to 1.20 mm. Other thicknesses or cutting methods should be confirmed according to circle diameter and order specification.
The listed coated-circle range includes PVDF, PE and other application-specific coating systems. Final selection depends on appearance, forming performance and end-use requirements.
The listed reference values are at least 22 µm for PVDF with varnish, at least 30 µm for PVDF without varnish and at least 18 µm for PE and other listed systems.
Yes. Custom color requirements can be discussed according to buyer details or an approved physical sample. Required gloss should also be specified where appearance consistency is important.
No. The coating must be selected and documented for the intended food-contact conditions. If the painted surface will directly contact food, provide the required market and service conditions before ordering.
Sample pieces can be discussed for checking color, coating appearance and material quality. For forming evaluation, the sample should match the intended alloy, temper, thickness and coating system as closely as possible.
The listed minimum order quantity is 1,000 kg per size. Final MOQ may depend on coating type, color, diameter and production requirements.
Please provide alloy, temper, diameter, thickness, coating type, coating thickness, color, gloss, coated side, finished application, forming requirement, quantity and destination.
Products
Application
Quick links
Contact Us