Alloy 1085 anodized aluminum sheet
DINGANG
7606125000
| Availability: | |
|---|---|
| Quantity: | |
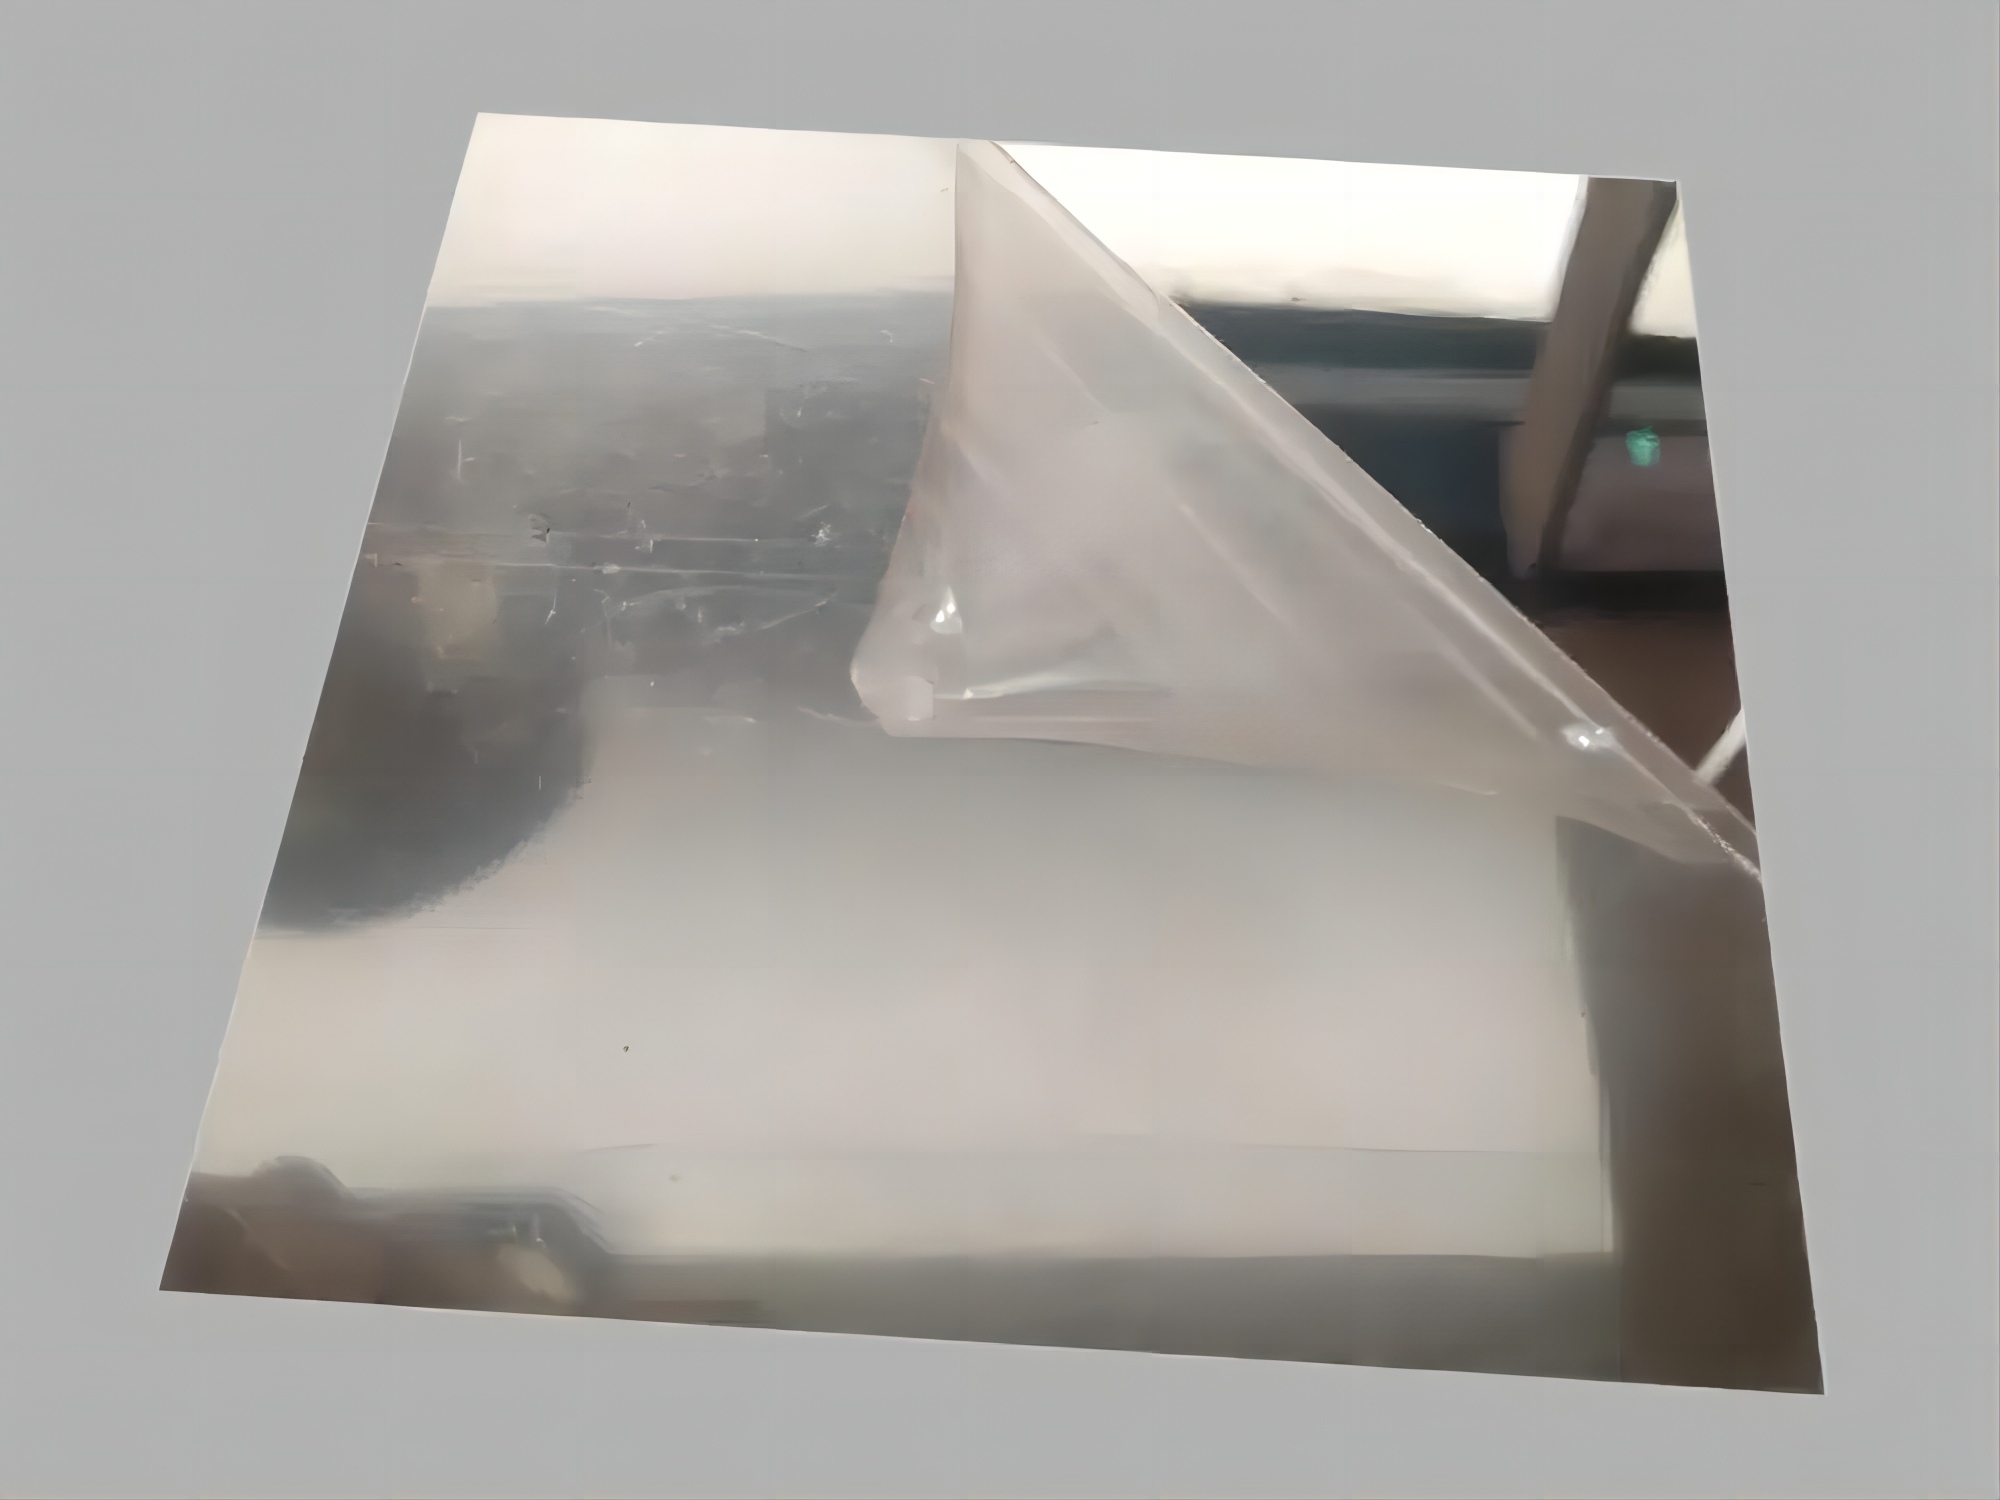
1085 anodized mirror aluminum sheet is a reflective aluminum material for lighting reflectors, decorative panels, display components, appliances and other applications requiring a bright metallic surface combined with the durability of an anodized finish.
The mirror surface is prepared before or as part of the finishing process, and anodizing then converts the aluminum surface into an integral aluminum oxide layer. Unlike a painted topcoat, the anodic layer is formed from the aluminum substrate itself and can subsequently be sealed or colored.
AA1085 is the primary material positioning for this product, while AA1060 and AA3003 are also listed as available options. Material can be supplied in thicknesses from 0.17 to 1.00 mm and standard widths of 1000, 1200 and 1250 mm.
Request Anodized Mirror Aluminum Price
| Product | Anodized mirror aluminum sheet |
| Primary Alloy | AA1085 |
| Other Listed Alloys | AA1060, AA3003 |
| Thickness | 0.17–1.00 mm |
| Standard Widths | 1000 mm, 1200 mm, 1250 mm |
| Surface | Mirror-finish aluminum with anodized surface treatment |
| Color | Natural mirror finish and customized anodized colors subject to process and sample confirmation |
| Listed Tensile Strength Reference | 130 MPa according to the existing product data; exact mechanical properties must be confirmed for the selected alloy and temper |
| Listed Yield Strength Reference | 115 MPa according to the existing product data; exact mechanical properties must be confirmed for the selected alloy and temper |
| Reflectance | To be specified and confirmed according to mirror grade, measurement method and end-use requirement |
| Anodic Film Thickness | To be agreed according to the required surface durability, color and application |
| Temper | To be confirmed according to alloy, required rigidity and forming process |
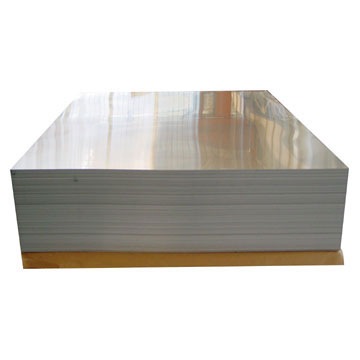
| Packing | Export-standard wooden pallets according to shipment requirements |
| Minimum Order Quantity | 1 metric ton according to specification |
| Payment Terms | 30% T/T deposit with 70% balance against the B/L copy, or 100% irrevocable L/C at sight according to the listed terms |
| Delivery Reference | Approximately 25 days after receipt of L/C or deposit, subject to final specification and production schedule |

Mirror aluminum is produced to create a bright, highly reflective metallic surface. Surface preparation, alloy purity, rolling quality, polishing and subsequent finishing all influence the final visual and optical result.
Anodizing is an electrochemical conversion process. The aluminum surface is converted into aluminum oxide rather than simply covered with a separate paint film. This anodic oxide becomes part of the aluminum surface and can then be sealed or colored.
A properly specified anodized surface provides increased resistance to corrosion and surface wear compared with untreated aluminum. Actual performance depends on anodic film thickness, sealing quality, alloy, environment and handling conditions.
The porous anodic layer can be colored before sealing. Natural silver mirror finishes and decorative anodized colors can therefore be discussed according to the required appearance and end-use environment.
AA1085 is commonly selected for mirror-finish aluminum where buyers prioritize a clean reflective surface. A high-purity aluminum substrate generally provides a more suitable starting surface for controlled mirror finishing than alloys selected primarily for higher mechanical strength.
For lighting and reflector applications, AA1085 should therefore be evaluated first when optical appearance is a major requirement. Final performance should still be confirmed by measured reflectance rather than alloy designation alone.
AA1060 can be considered for suitable reflective and decorative applications where good surface quality, formability and commercial availability are important. Reflective performance should be confirmed on the approved production sample.
AA3003 provides higher strength than commercially pure aluminum grades and can be evaluated for decorative panels or fabricated components where mechanical rigidity is more important. Its surface appearance and measured reflectance should be approved separately.
Discuss 1085, 1060 or 3003 Material
A mirror appearance alone does not define optical performance. Two sheets can both look bright to the eye while producing different measured reflection characteristics.
For LED lighting, luminaires, display backlighting or other optical applications, the buyer should specify the required reflectance together with the test method and whether total, specular or diffuse reflection is important.
| Optical Requirement | Why It Matters |
| Total Reflectance | Indicates the overall amount of incident light reflected by the surface |
| Specular Reflectance | Important where light must be reflected in a controlled mirror-like direction |
| Diffuse Reflectance | Relevant where a softer or more distributed reflected-light pattern is required |
| Measurement Method | Should be agreed so supplier and buyer are comparing values measured under the same conditions |
| Production Sample | Allows visual appearance and measured optical performance to be approved before bulk production |
| Material Type | Main Characteristic | Typical Selection Basis |
| Polished / Mirror Aluminum | Bright reflective surface produced through rolling, polishing or other mirror-finishing processes | Decorative appearance and general reflective applications |
| Anodized Mirror Aluminum | Mirror surface combined with an integral anodic oxide layer | Reflective appearance plus improved surface durability and corrosion resistance |
| High-Reflective Optical Aluminum | Engineered surface system with controlled optical performance | Applications requiring a specified measured reflectance rather than mirror appearance alone |
| Colored Anodized Mirror | Reflective metallic appearance combined with anodized coloration | Decorative interiors, displays, furniture and appearance-driven components |
The existing process flow for this product includes surface preparation, polishing, anodizing, washing and sealing. Actual production parameters can vary according to alloy, mirror grade, anodic-film requirement and color.

| Step | Existing Process Reference |
| 1 | Mechanical polishing |
| 2 | Degreasing |
| 3 | Washing |
| 4 | Chemical polishing |
| 5 | Washing |
| 6 | Anodizing |
| 7 | Washing |
| 8 | Sealing |
| 9 | Final mechanical brightening according to the existing process description |
The anodic oxide layer is porous before sealing. Sealing closes or stabilizes the pore structure and is an important part of achieving the required corrosion resistance and long-term surface performance.
For colored anodized mirror sheet, coloring normally takes place before sealing. Buyers requiring controlled color appearance should approve both the color and mirror effect on a physical production sample.
Flatness directly affects the visual quality of a mirror surface and the direction of reflected light. Buyers using the material in lighting, displays or large decorative panels should specify acceptable flatness rather than relying only on thickness and width.
Minor scratches, dents and pressure marks can be highly visible on a mirror finish. Surface acceptance criteria and protective handling should therefore be agreed before shipment.
Visible differences in polishing, gloss or anodizing can create inconsistent reflection across adjacent parts. For high-appearance projects, production lots should be compared with an approved reference sample.
Oil, fingerprints, residue and abrasive contamination should be avoided during processing and installation. Cleaning methods must be compatible with the anodized surface.
Mirror aluminum surfaces require careful handling because cosmetic defects are more visible than on matte or mill-finish material. Where protective film is required, the film specification should be agreed according to subsequent cutting, stamping, bending, storage and installation conditions.
Sheets should be stored in a clean, dry environment and separated from abrasive particles. Operators should avoid dragging one mirror surface across another during handling.
Request Mirror Surface Samples
Anodized mirror aluminum sheet can be cut into reflector blanks, decorative panels and other components. Tooling and work surfaces should be kept clean to avoid scratching the mirror face.
Forming performance depends on alloy, temper, thickness, bend radius and anodic-film condition. For reflectors or decorative components with significant deformation, the proposed part should be trialed before bulk production.
Tight bending can place high strain on both the aluminum substrate and anodized surface. Buyers should provide the required bend angle and inside radius so a suitable alloy and temper can be reviewed.
Where the sheet will be bonded to another substrate, adhesive compatibility should be tested against the actual anodized or reverse-side surface before mass production.
Anodized mirror aluminum can be evaluated for LED luminaires, reflector panels, downlights, display lighting and other lighting components. The required total or specular reflectance should be stated in the purchase specification.
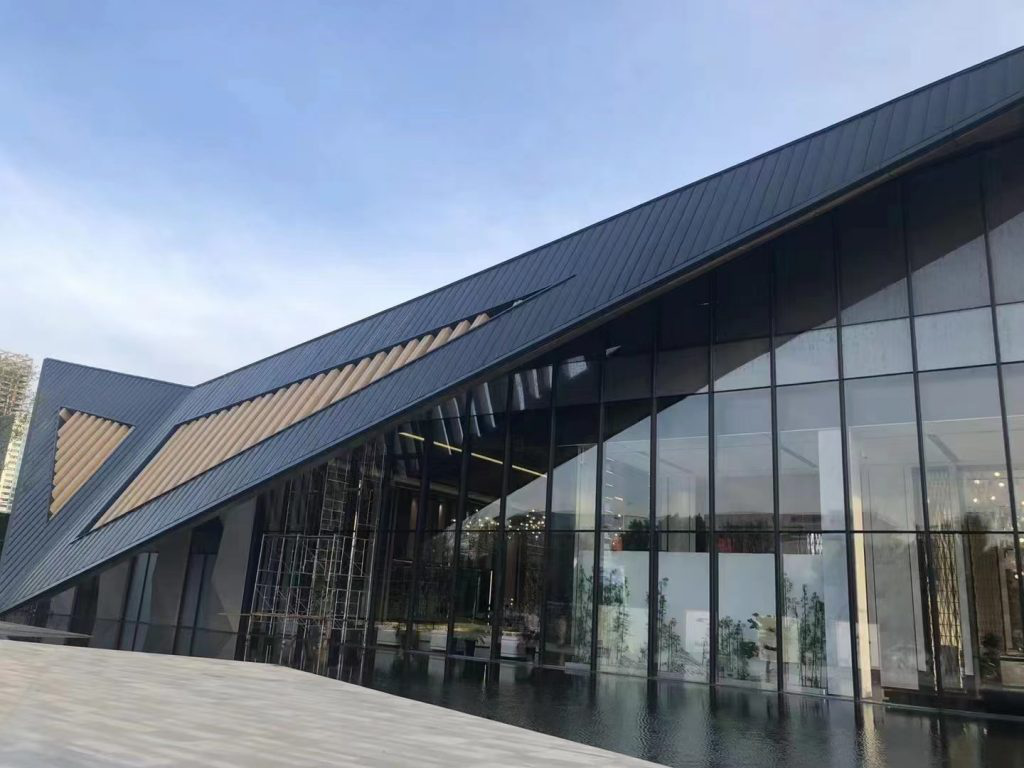
Mirror aluminum can be used for decorative wall panels, ceilings, feature panels, display areas and other architectural components where a lightweight reflective metallic appearance is required.
Reflective anodized aluminum can be used for suitable cabinet doors, furniture inserts, display furniture and decorative surfaces where the selected thickness and mounting system meet the design requirements.
The material can be considered for decorative appliance panels, bezels and reflective components where a metallic mirror finish and anodized surface are required.
Mirror aluminum can be used in display backgrounds, illuminated signage, retail fixtures and branded decorative panels where reflected light or a premium metallic appearance is part of the design.
Anodized mirror aluminum can be evaluated for selected non-safety-critical decorative trim and appearance components. Optical rear-view mirrors and other regulated vehicle components require separate approved specifications and should not be substituted with decorative mirror sheet without engineering validation.

Confirm alloy and temper before cutting or forming. The same thickness can behave differently depending on the selected material condition.
Verify sheet thickness and usable width against the approved specification. Current listed widths are 1000, 1200 and 1250 mm.
For lighting and optical applications, inspect and measure reflectance according to the agreed test method rather than approving material only by visual brightness.
Inspect for scratches, polishing lines, dents, stains, haze, color variation and localized surface defects that could affect decorative or optical performance.
Where anodic-film thickness, sealing performance or color is critical, include the required value and inspection method in the approved purchase specification.
For stamped reflectors, bent decorative panels or other formed components, produce a representative trial using the intended tooling before approving bulk production.
Request Material for a Reflector Trial
State whether the material will be used for a lighting reflector, decorative wall, ceiling, furniture panel, appliance component, display or another application.
AA1085 is the primary choice for this product. AA1060 and AA3003 are also listed and can be evaluated where forming, mechanical strength, surface appearance or commercial requirements differ.
Provide the required temper if already specified, or provide the finished component and forming process so the required rigidity and formability can be reviewed.
The listed thickness range is 0.17–1.00 mm and the listed standard widths are 1000, 1200 and 1250 mm. Provide finished dimensions and dimensional tolerances for final confirmation.
For functional reflectors, specify the required total, specular or diffuse reflectance and the applicable measurement method. Do not rely only on the description “mirror finish.”
Specify natural mirror or the required anodized color together with any anodic-film, sealing or surface-durability requirement.
State acceptable limits for scratches, dents, polishing lines, haze, color variation and other visible defects, particularly for lighting and high-appearance decorative applications.
Provide the intended cutting, stamping, bending, drilling or bonding process so the selected alloy, temper and anodized finish can be reviewed against the required fabrication.
| Minimum Order Quantity | 1 metric ton according to specification |
| Payment | 30% T/T deposit with 70% balance against the B/L copy, or 100% irrevocable L/C at sight according to the listed terms |
| Delivery Reference | Approximately 25 days after receipt of L/C or deposit, subject to final production specification |
| Packing | Export-standard wooden pallets with surface and edge protection according to shipment requirements |
| Recommended Inquiry Information | Application, alloy, temper, thickness, width and length, reflectance requirement, anodizing requirement, color, surface acceptance, fabrication process, quantity and destination |
It is aluminum with a reflective mirror-like surface followed by anodizing, which converts the surface into an integral aluminum oxide layer to improve surface durability and corrosion resistance.
AA1085 is a high-purity aluminum grade commonly selected for mirror finishing where clean surface quality and reflective performance are important. Final optical performance should still be confirmed by measurement.
The current product specification also lists AA1060 and AA3003. Their suitability depends on required reflectivity, forming, strength and finished appearance.
The current listed thickness range is 0.17–1.00 mm.
The current listed standard widths are 1000 mm, 1200 mm and 1250 mm.
The existing specification for this product does not state a single guaranteed reflectance value. Buyers requiring optical performance should specify the required reflectance and test method for confirmation before ordering.
No. A visually bright mirror finish does not by itself define total, specular or diffuse reflectance. Functional reflector applications should use measured optical values.
Yes, it can be evaluated for compatible LED and lighting reflector components. The required reflectance, surface geometry, forming process and thermal environment should be specified before material approval.
It can be bent when the alloy, temper, thickness, bend radius and anodized surface are compatible with the required geometry. Tight bends should be trialed before mass production.
Stamping can be evaluated for suitable reflector geometries. Buyers should provide forming depth, part drawing and temper requirements so the material can be reviewed before production.
Customized colors can be discussed according to the anodizing process and approved physical sample. Color, mirror effect and sealing requirement should be approved together.
The anodic oxide is formed from the aluminum surface and is integral with the substrate rather than being applied as a separate paint film. Surface damage is still possible through severe abrasion, impact or unsuitable processing.
Anodizing improves corrosion resistance, but performance still depends on anodic-film quality, sealing, environment, cleaning chemicals, edges and long-term exposure conditions.
Confirm alloy, temper, thickness, reflectance type and value, test method, flatness, surface-defect criteria, anodizing requirement, forming process and protective-film requirement.
The current product information lists a minimum order quantity of 1 metric ton according to specification.
The existing product information lists approximately 25 days after receipt of L/C or deposit. Actual lead time depends on alloy, dimensions, anodizing, color and quantity.
Please provide application, alloy and temper if known, thickness, width and length, required reflectance and measurement method, anodic-film requirement, color, fabrication process, surface quality requirement, quantity and destination.
Products
Application
Quick links
Contact Us